Extreme weather events increase the need for continuous environmental monitoring and early detection of critical changes. However, installing measurement technology in remote or hard-to-reach locations presents a fundamental challenge: How can sensors collect and transmit data reliably when there is no connection to the power grid?
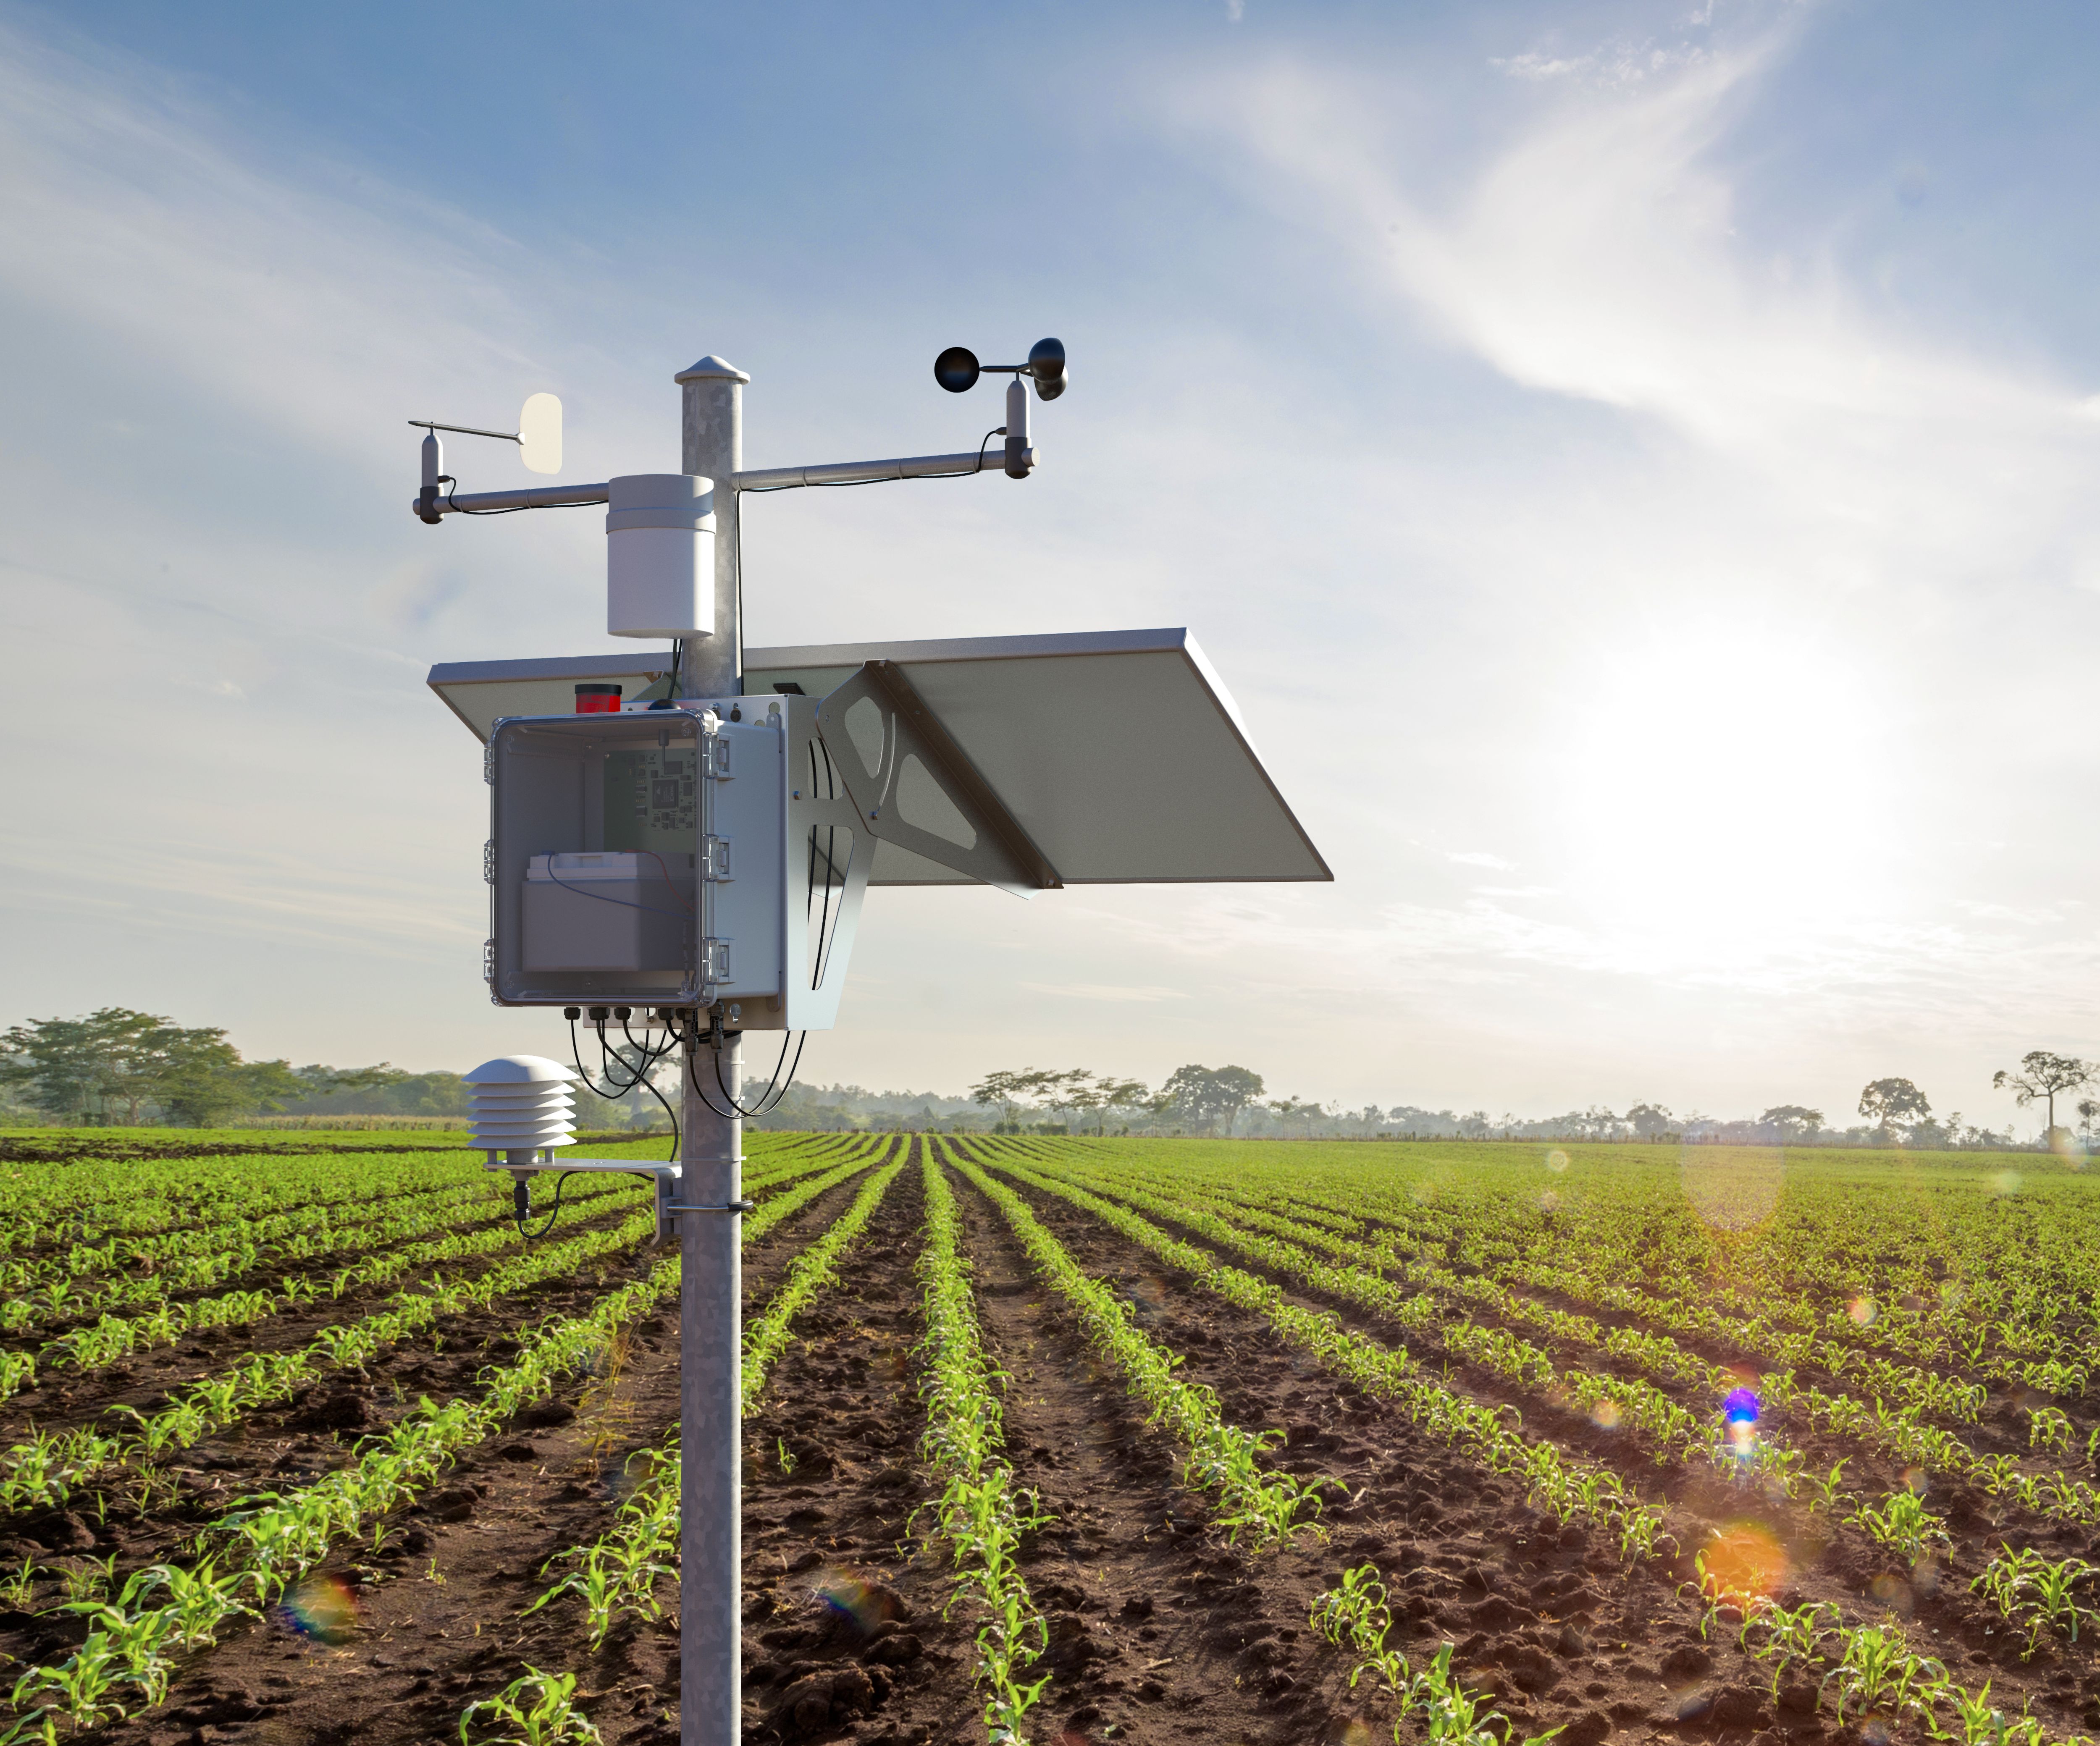
The POS Pico off-grid system addresses this challenge with a photovoltaic panel, outdoor housing, battery storage, and flexible mounting components. Together, they create an energy-self-sufficient monitoring system for remote field applications.
Figure 1: Reliable data acquisition in any weather with an energy-self-sufficient measurement system.Continue reading →
Compact machines, decentralized units, and shorter commissioning times are increasing the pressure on industrial connection technology. Manufacturers need to use less installation space and fewer cables without compromising operational safety. Standardized hybrid connectors provide an effective answer by combining power, signals, and data within a single interface.
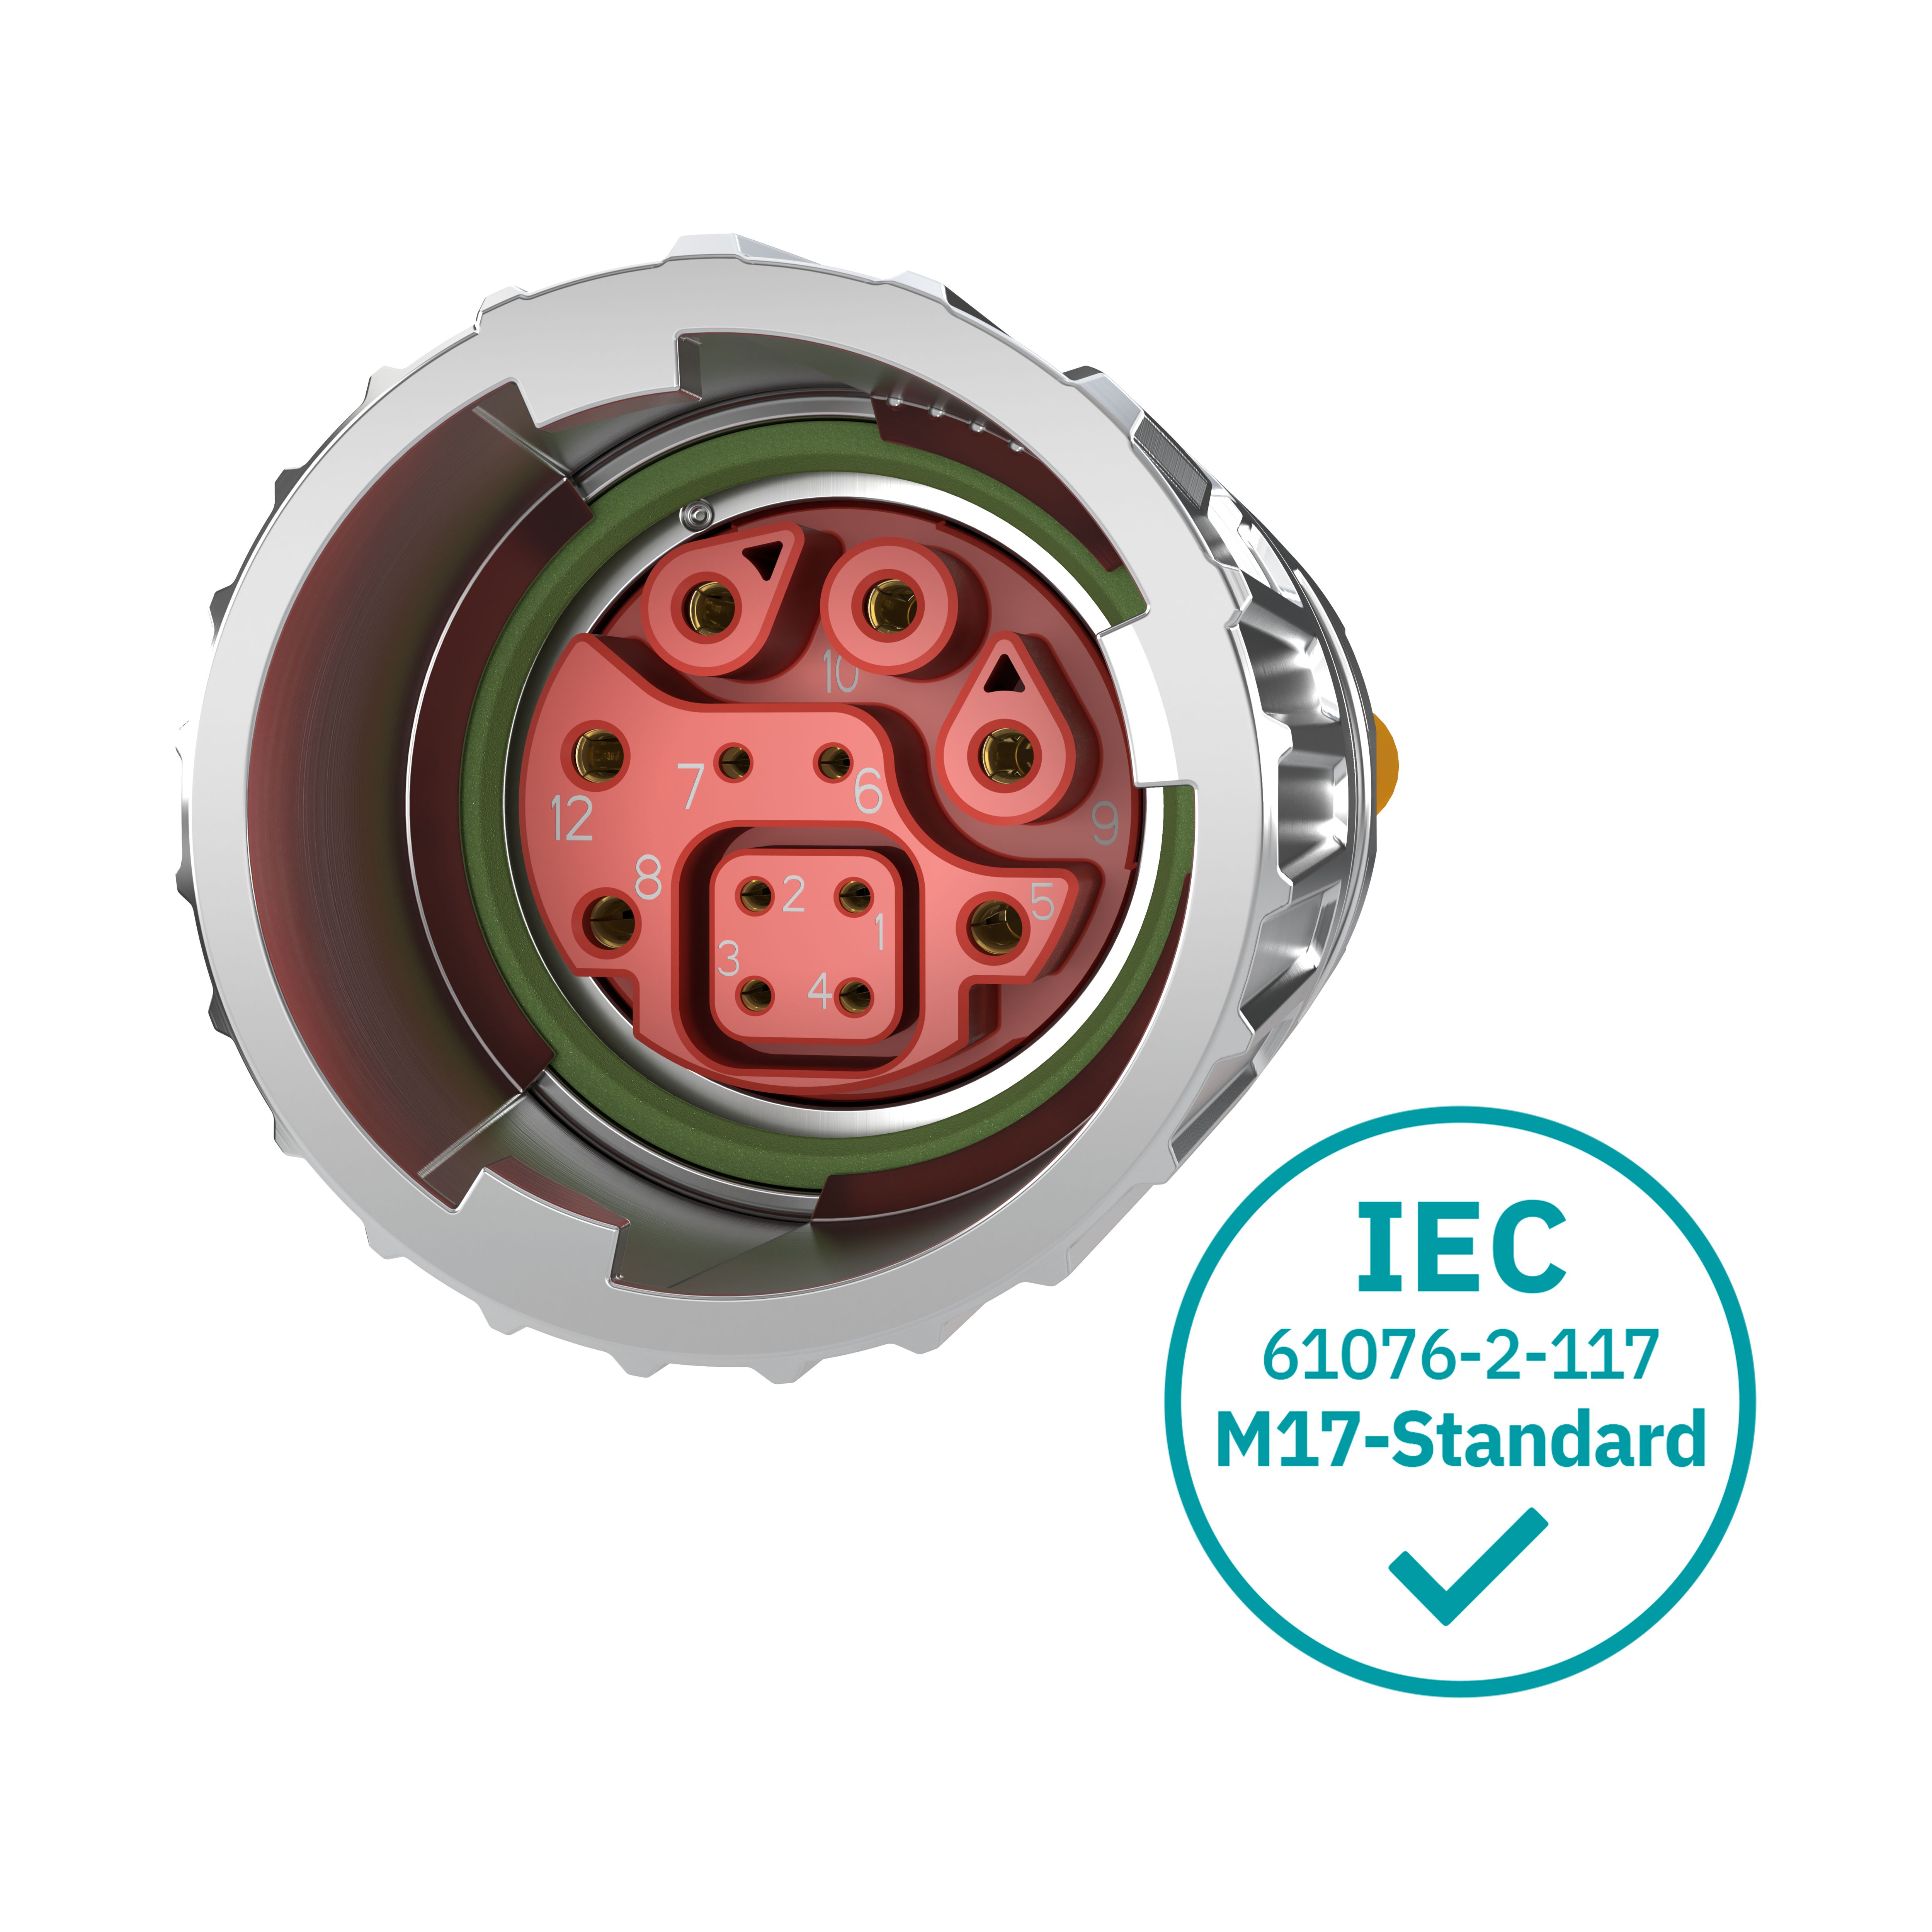
Hybrid one-cable solutions in machine and system cabling: standardized interfaces replace proprietary approaches and save installation space.
Why standardized hybrid connectors matter
Traditional machine wiring often requires separate cables for power and for signals or data. That architecture occupies valuable space, uses more material, and extends installation time. Hybrid one-cable solutions reduce these requirements. However, many existing solutions are proprietary, limiting compatibility between manufacturers.
Standardization addresses this challenge. International standard IEC 61076-2-117 defines requirements for shielded hybrid circular connectors in sizes from M12 to M40. These requirements include the mechanical interface, electrical characteristics, EMC performance, standard and fast locking, and degrees of protection up to IP67.
As a result, standard-based components can reduce dependence on individual vendors and simplify global procurement. Clearly defined interfaces also support long-term machine availability, spare-part planning, and future device development.
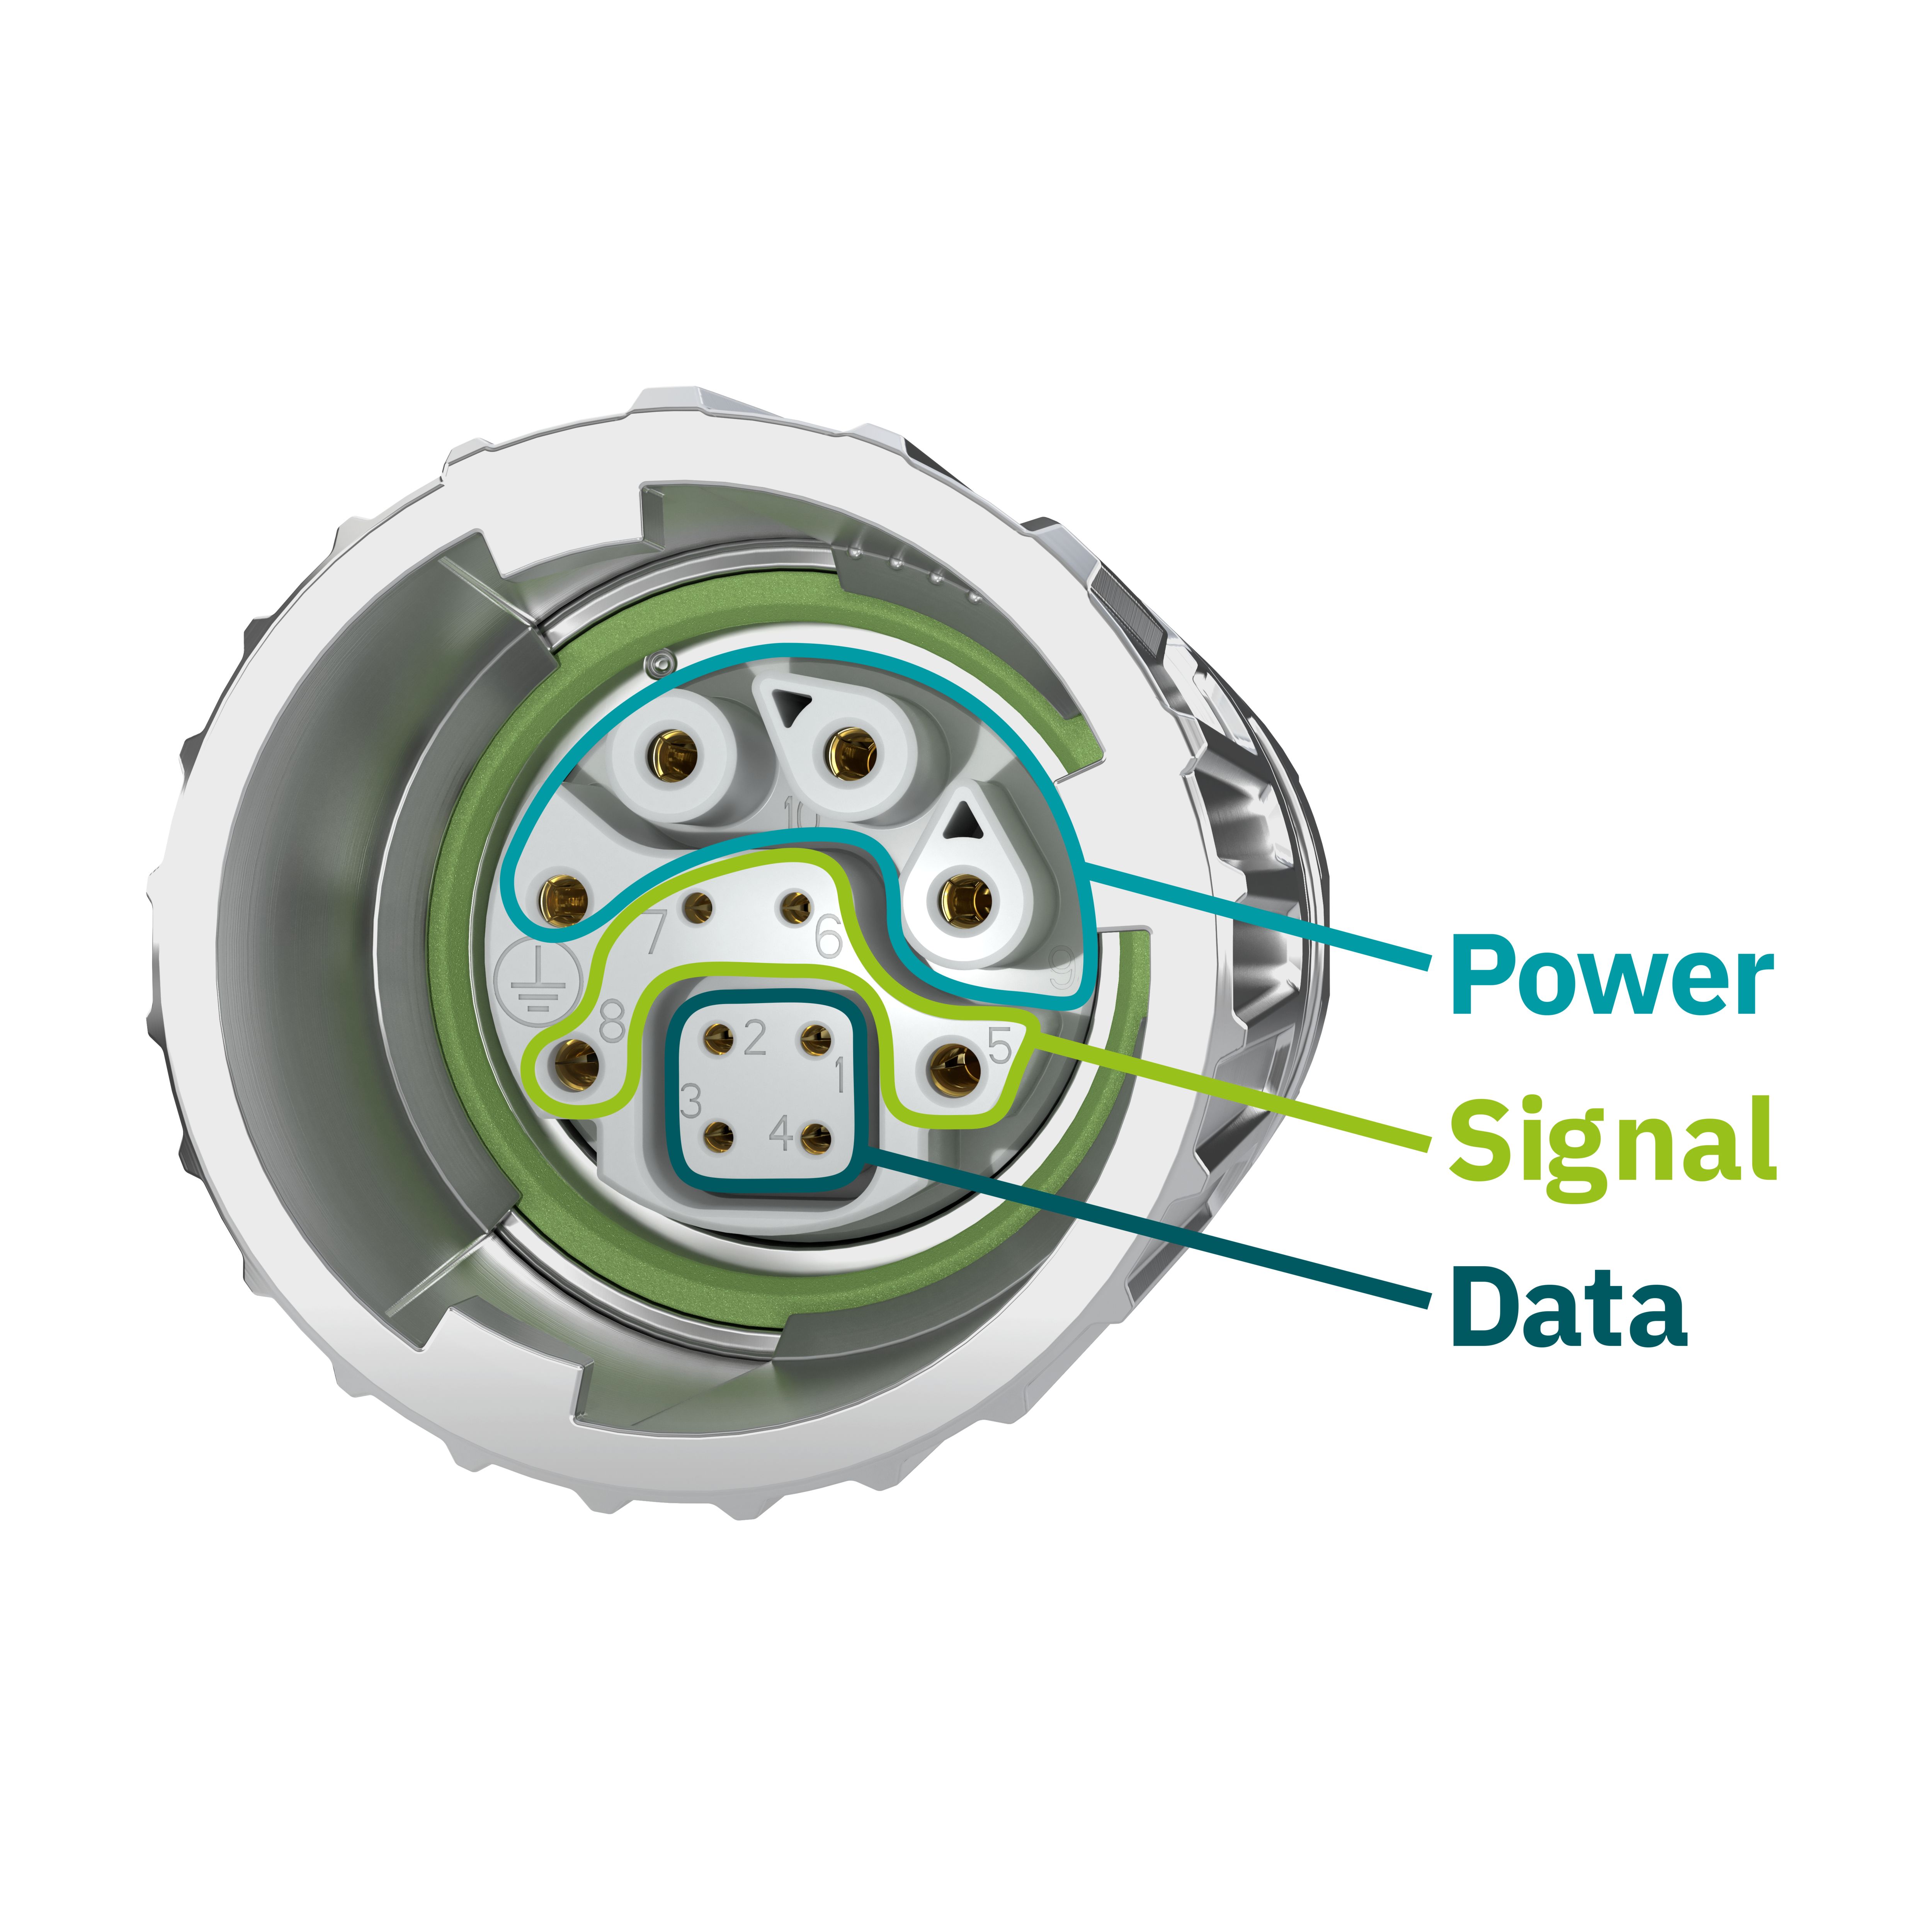
Three functions in one compact interface
The M17 PRO HYBRID is the first product in the M17 format designed in accordance with IEC 61076-2-117. It transmits power, signals, and data through one compact circular connector. Device developers can therefore use fewer interfaces, simplify system layouts, and reduce assembly and material requirements without sacrificing functionality.
The standard covers both the pin connector pattern and the connection thread. This establishes compatibility on the device and pin connector pattern sides while still allowing manufacturers some flexibility in the field-side realization of fast-locking systems.
Faster and safer installation
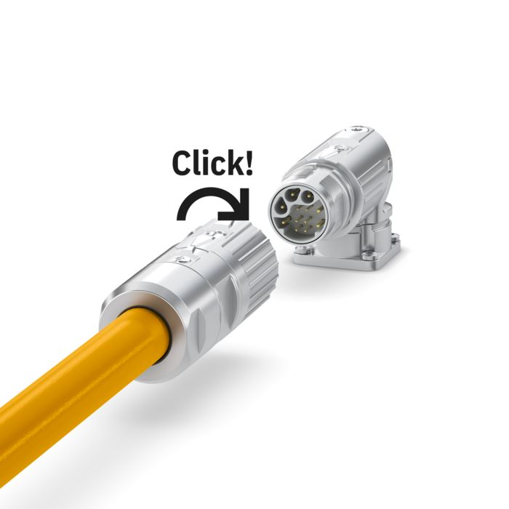
Phoenix Contact uses that flexibility in its patented ONECLICK fast-locking system. One click indicates that the connector has reached the correct locking position. Tactile and visual feedback provide additional confirmation. Depending on the application, this design can reduce connection time by up to 70% compared with traditional metric screw locking mechanisms.
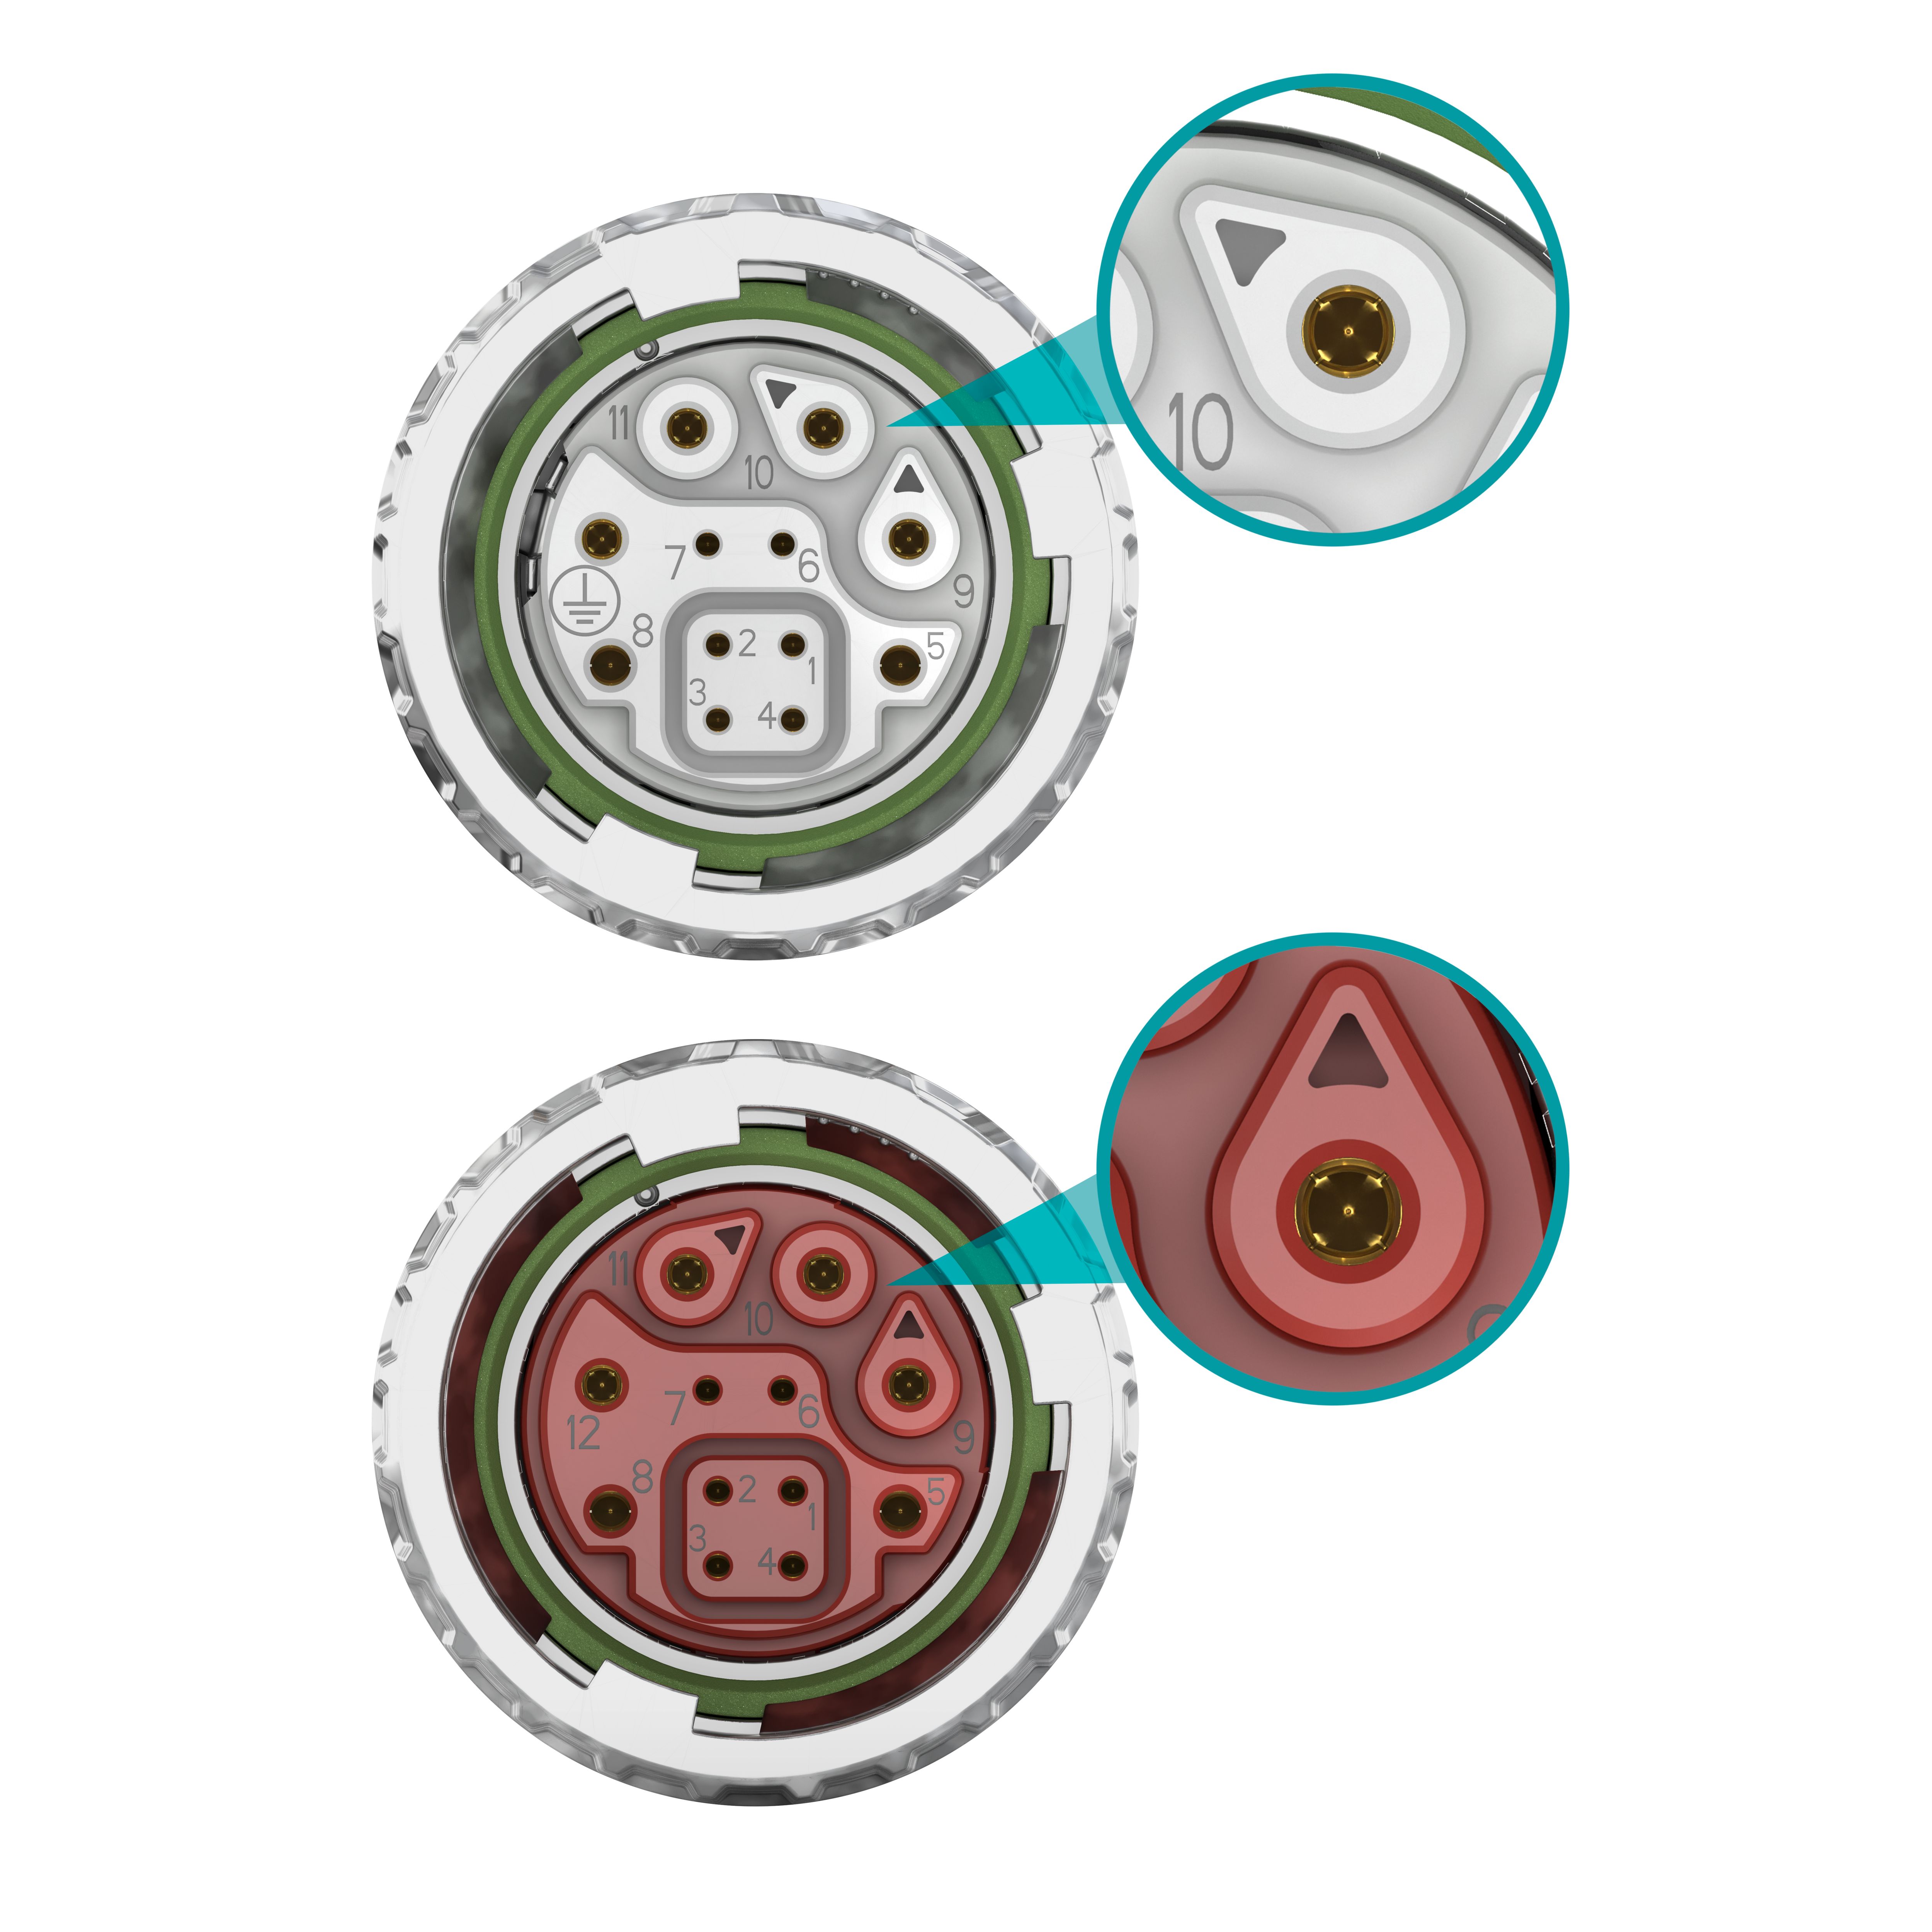
Integrated touch protection on the power contacts enables the safe use of connector and socket inserts on device and field connectors. It also simplifies series connections in a daisy chain, reducing the need for complex parallel wiring.
Mechanical and color coding help prevent incorrect connections. They distinguish the 50 V Type 2B version from the 630 V Type 2 version defined by IEC 61076-2-117. This clear assignment supports safer installation, maintenance, and replacement.
Compact dimensions without sacrificing performance
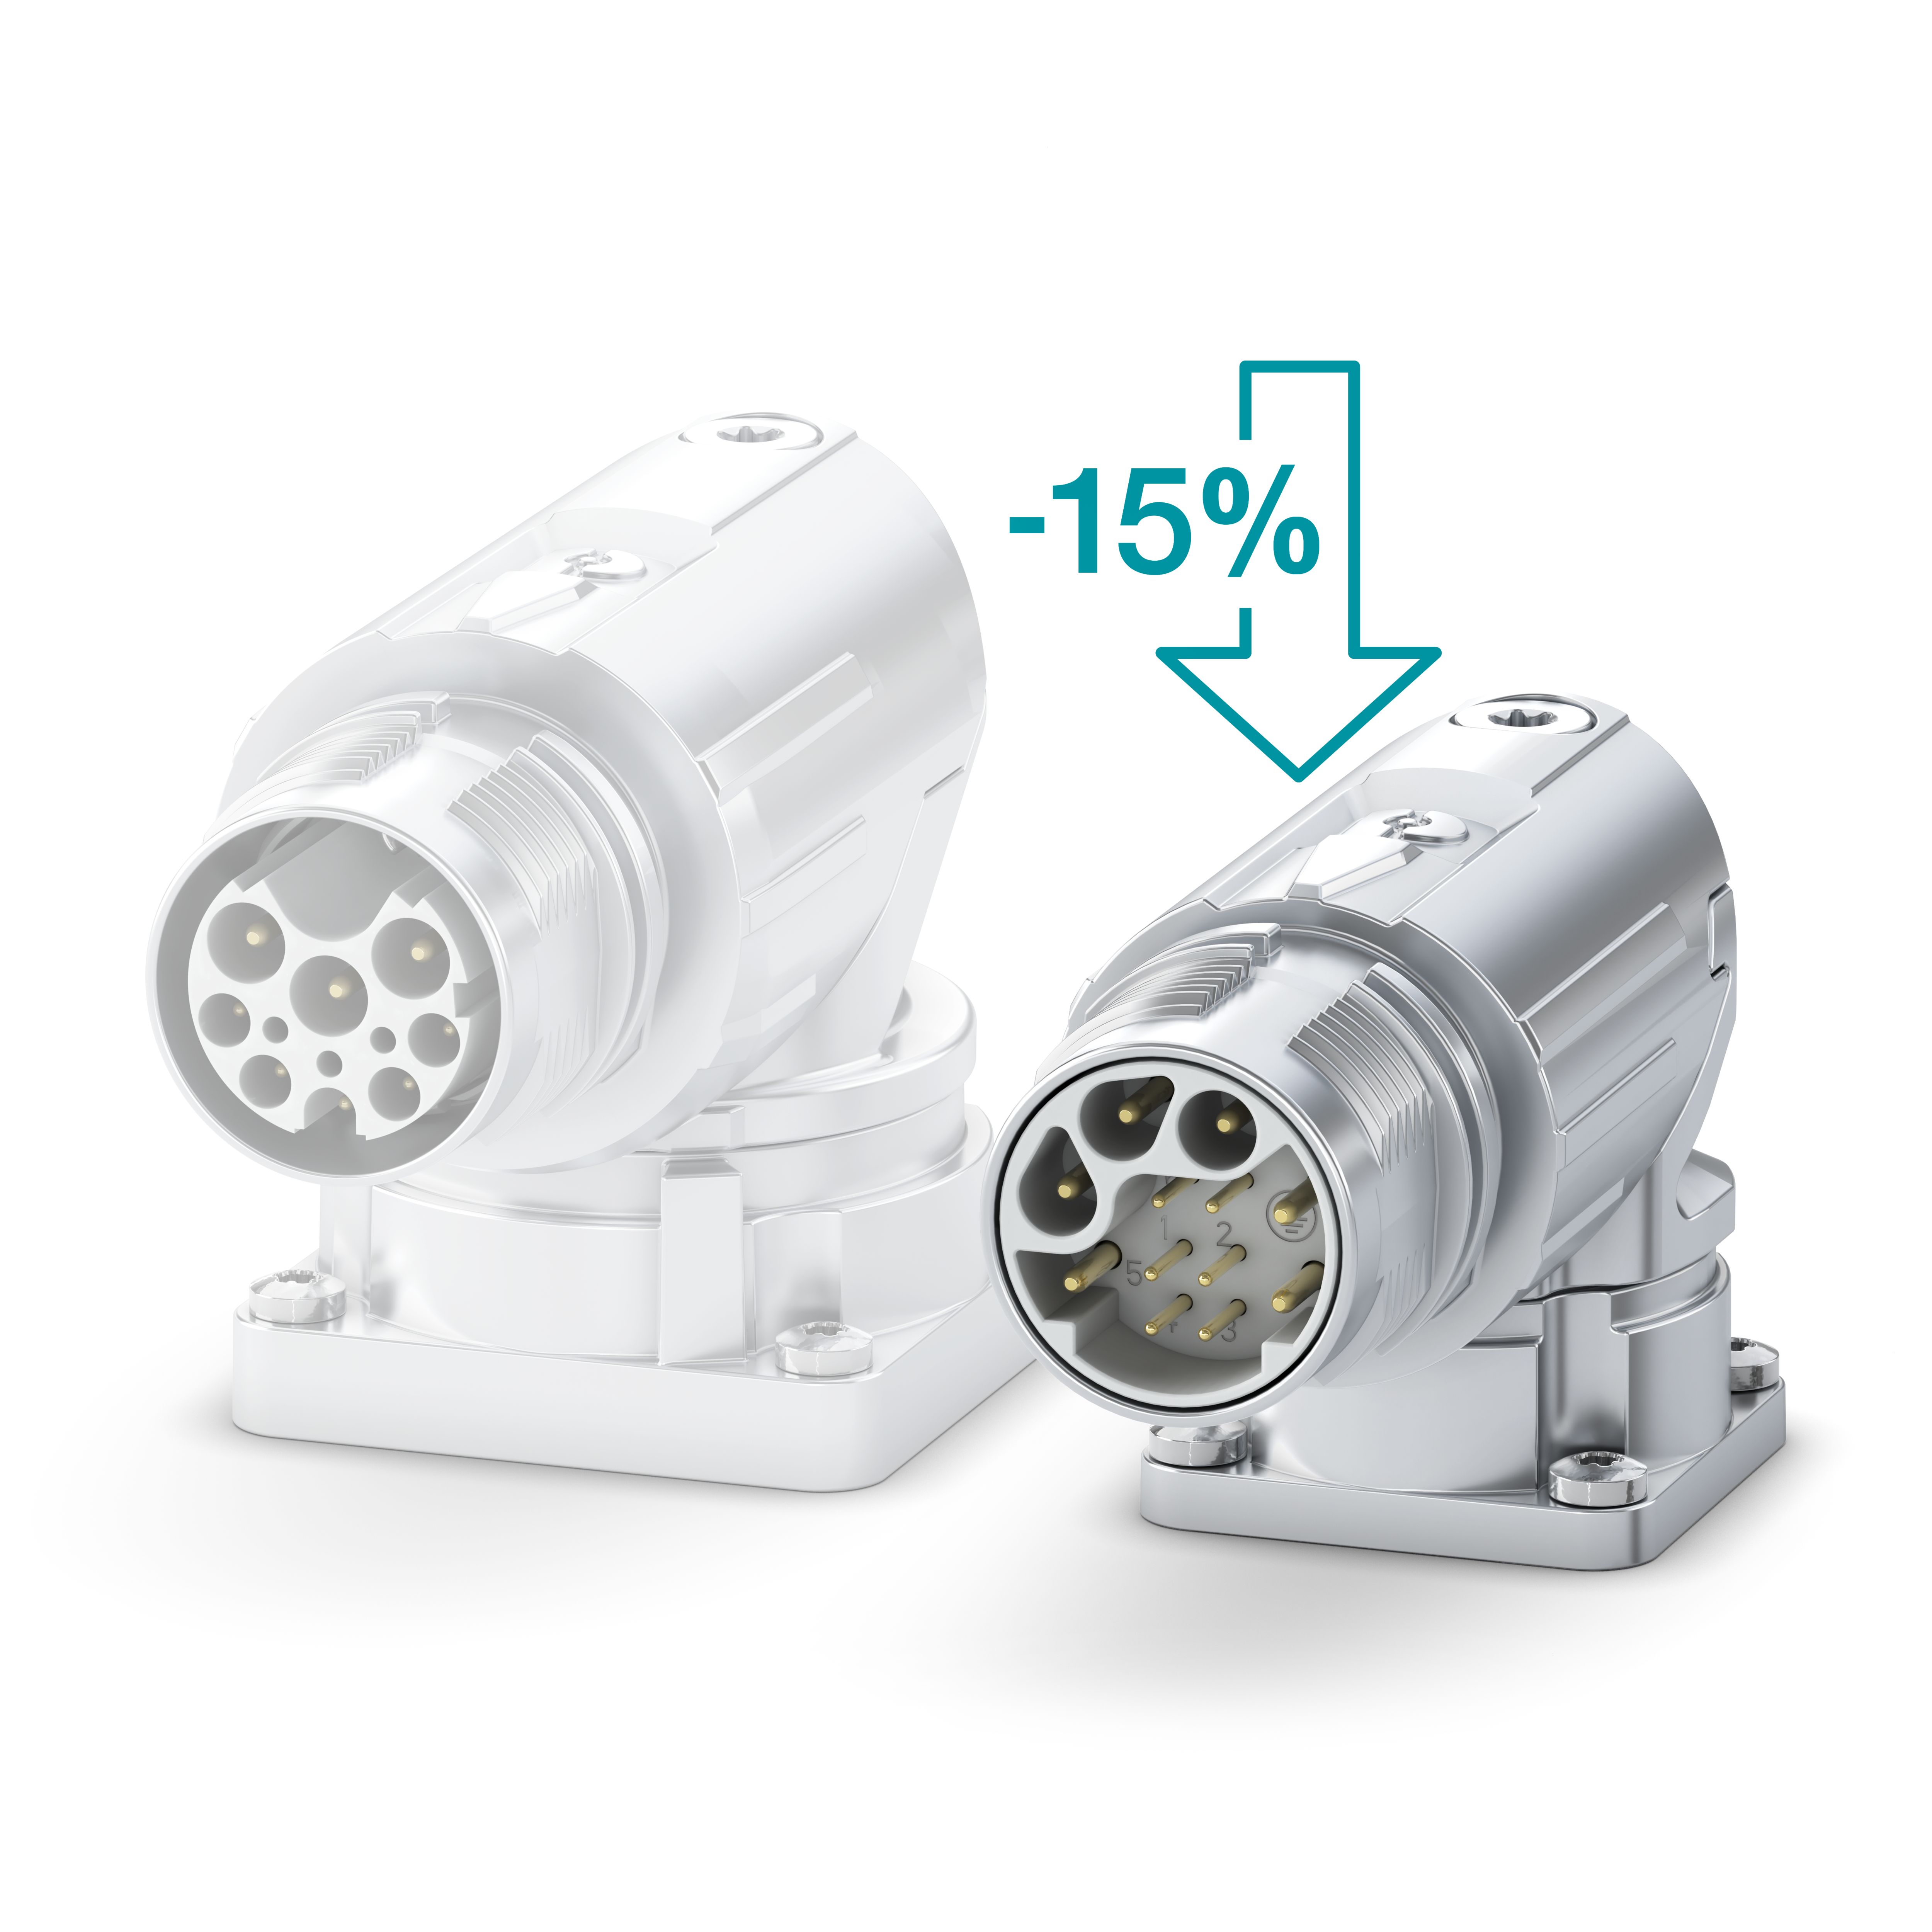
Angled device plugs reduce the installed height by approximately 15% compared with standard M17 device plugs, bringing it to around 30 mm. A 21.6 × 21.6 mm flange option is available for straight and angled rotatable device plugs.
Despite its compact construction, the connector’s power contacts support conductor cross-sections up to 1.5 mm² and currents of up to 16 A per contact. Additional signal and data pins can integrate sensors, feedback signals, or communication into the same interface.
Built for demanding industrial applications
The M17 PRO HYBRID is designed to withstand vibration, shock, and temperature in industrial environments. Potential applications include industrial automation, robotics, mobile machinery, ventilation and building systems, automated guided vehicle wheel drives, collaborative robots, compact control units, and decentralized low-voltage drives.
For modular systems, standardized hybrid connectors offer a practical combination of compatibility, compact design, and faster mounting. By bringing power, signals, and data together, they can improve planning reliability while helping manufacturers build scalable machine concepts around predictable interfaces.
The M17 PRO HYBRID combines power, signals, and data in one compact connector designed in accordance with IEC 61076-2-117. Standardization, ONECLICK fast locking, clear coding, compact dimensions, and support for demanding industrial environments make it suitable for modular and decentralized machine concepts.
Explore the M17 hybrid connector portfolio and learn how standardized one-cable connectivity can support compact machine designs: www.phoenixcontact.com/M17hybrid
Carbon neutrality and decarbonization are reshaping industrial energy strategy. The All Electric Society vision describes a future in which renewable electrical energy is available in sufficient quantities and at affordable prices. Reaching that goal requires sector coupling, intelligent energy management, and more efficient power distribution. DC grids in industry offer a practical route forward.
Why move toward a DC Factory?
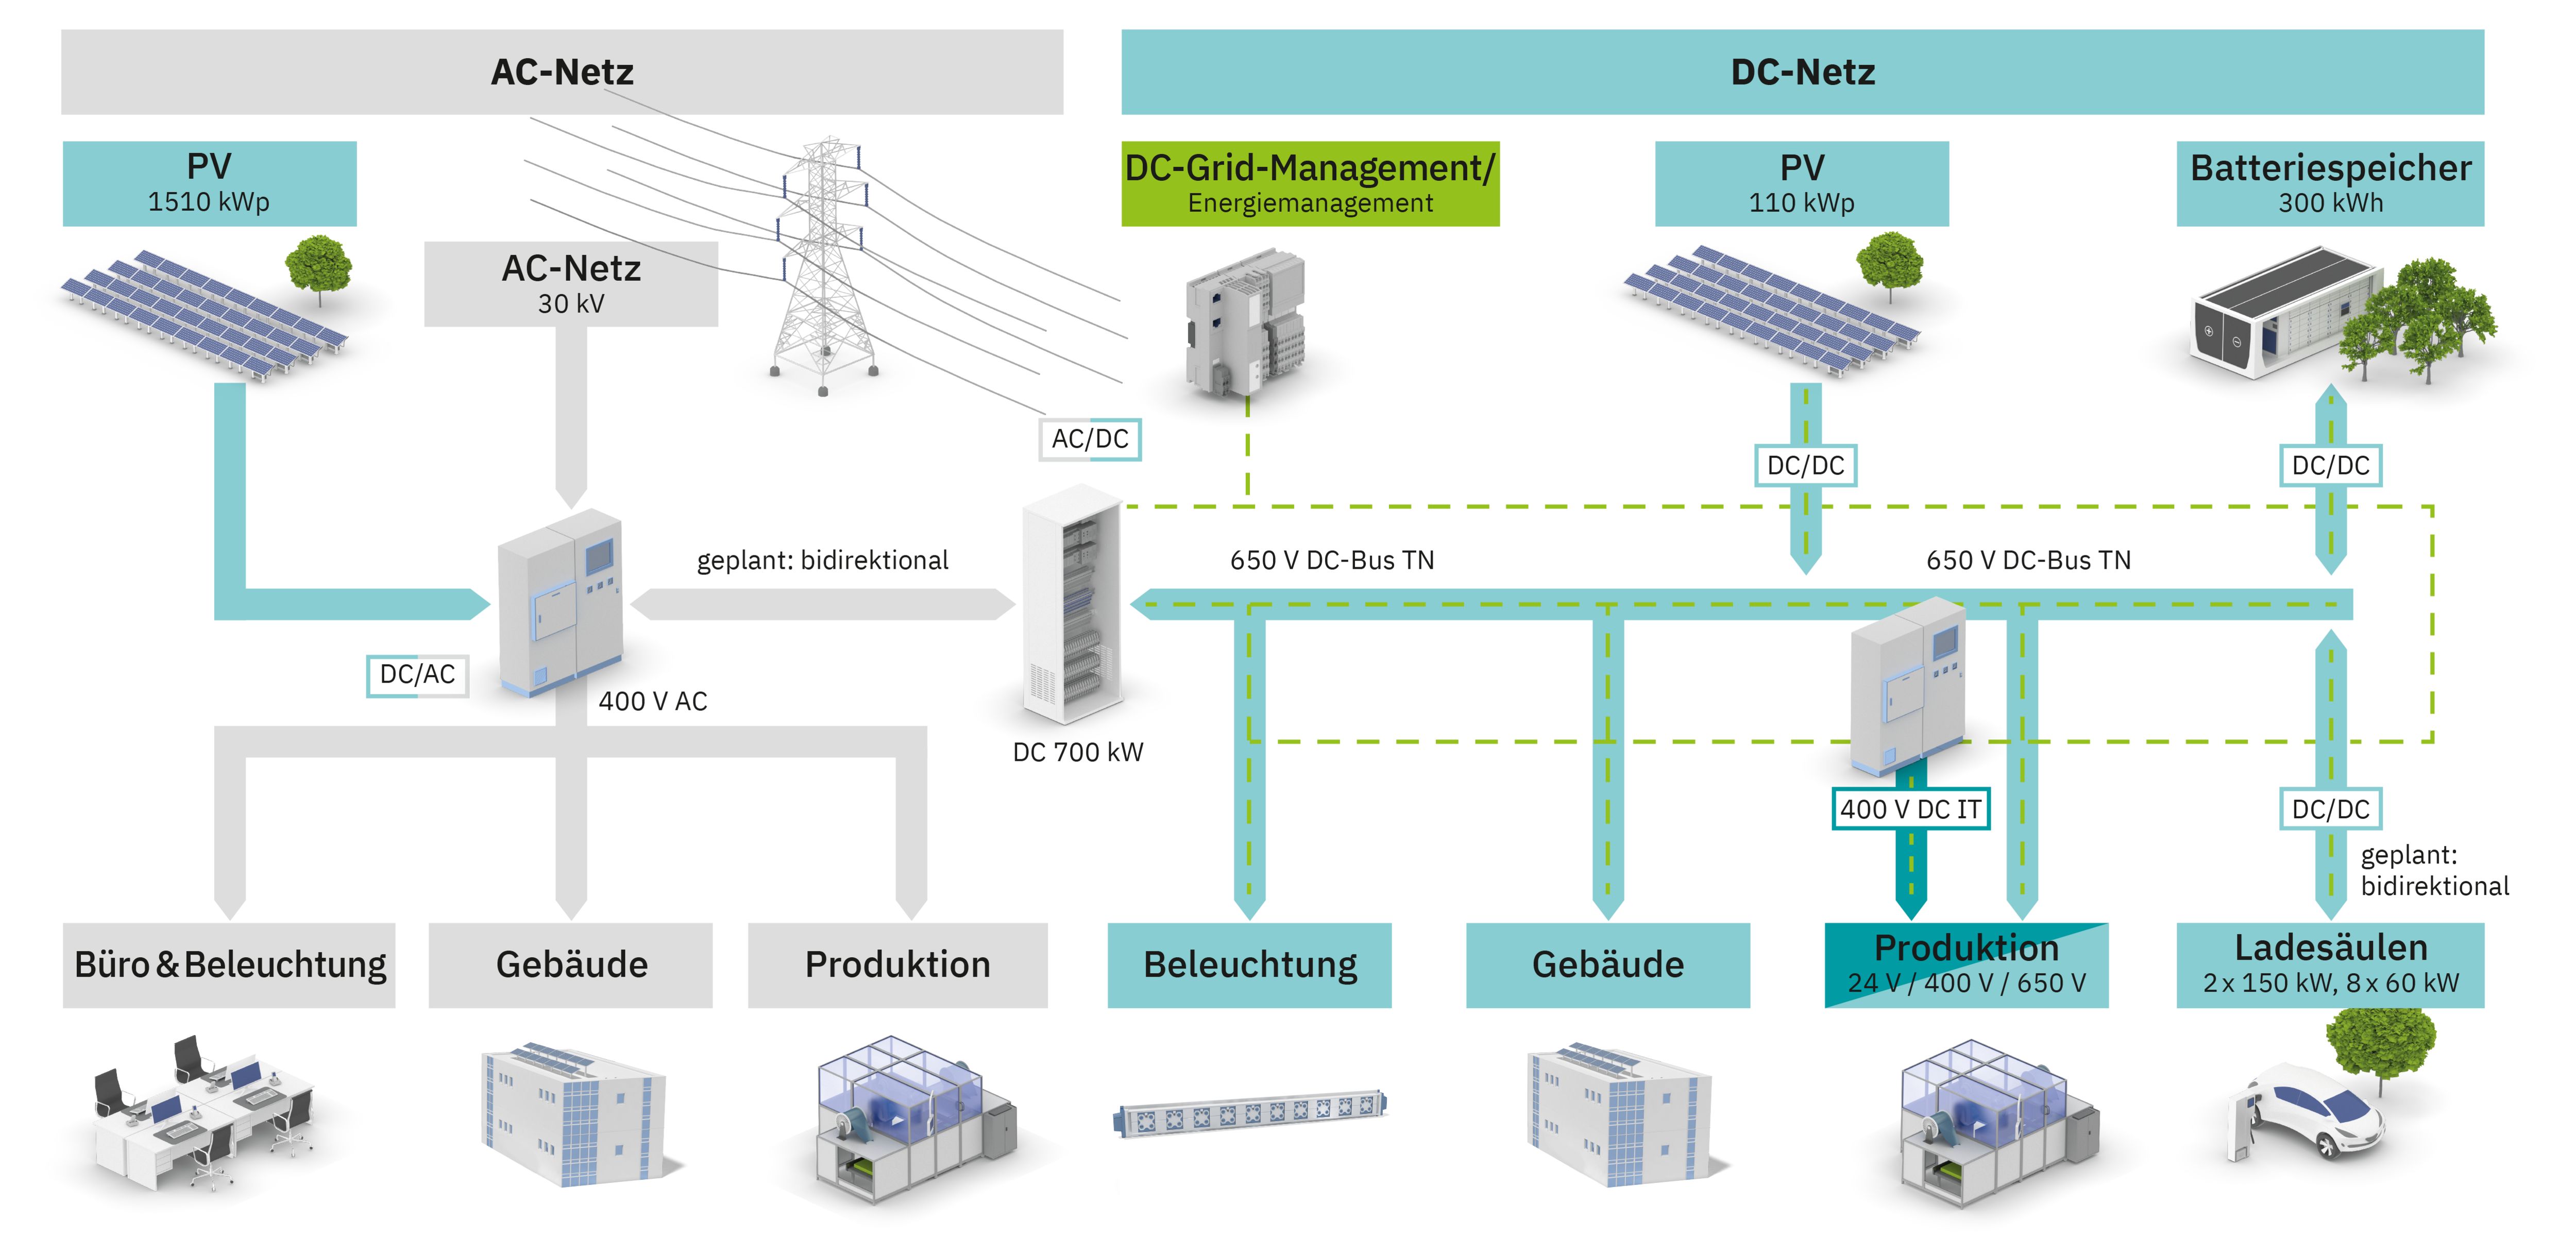
A factory DC grid can improve energy efficiency by recovering braking energy and reducing conversion losses. It can also integrate photovoltaic systems, battery storage, and EV charging stations directly. In suitable applications, recuperation can balance peak loads substantially, while fewer cables can reduce copper consumption.
The economic case is therefore compelling. However, a successful DC factory needs more than efficient components. It requires a coordinated concept covering objectives, topology, converters, protection, arc analysis, and energy management.
Start with objectives and operating conditions
Phoenix Contact’s All Electric Society Factory concept in Blomberg, Germany
Planning begins by defining what the DC grid must achieve. Engineers should evaluate recuperation potential from robots or storage and retrieval machines, required security of supply, connected loads, charging infrastructure, base loads, and startup peaks. Weather forecasts and electricity market prices may also influence the preferred energy strategy.
Fire protection, safety, and cybersecurity guidelines require equal attention. These inputs support an initial assessment of economic viability and risk before the project moves into detailed design.
Select the topology and voltage level
According to the ODCA and VDE SPEC 90037, normal operation takes place within a nominal band of 620 V to 750 V. This range balances component selection, losses, control reserves, and safety requirements.
A central DC busbar forms the power backbone. AC/DC coupling connects the factory to the AC grid, while DC/DC couplings integrate PV, battery storage, EV charging, lighting, and production equipment. Zoning, field distributors, or redundant feeds can add selectivity and resilience.
Design conversion, grounding, and protection together
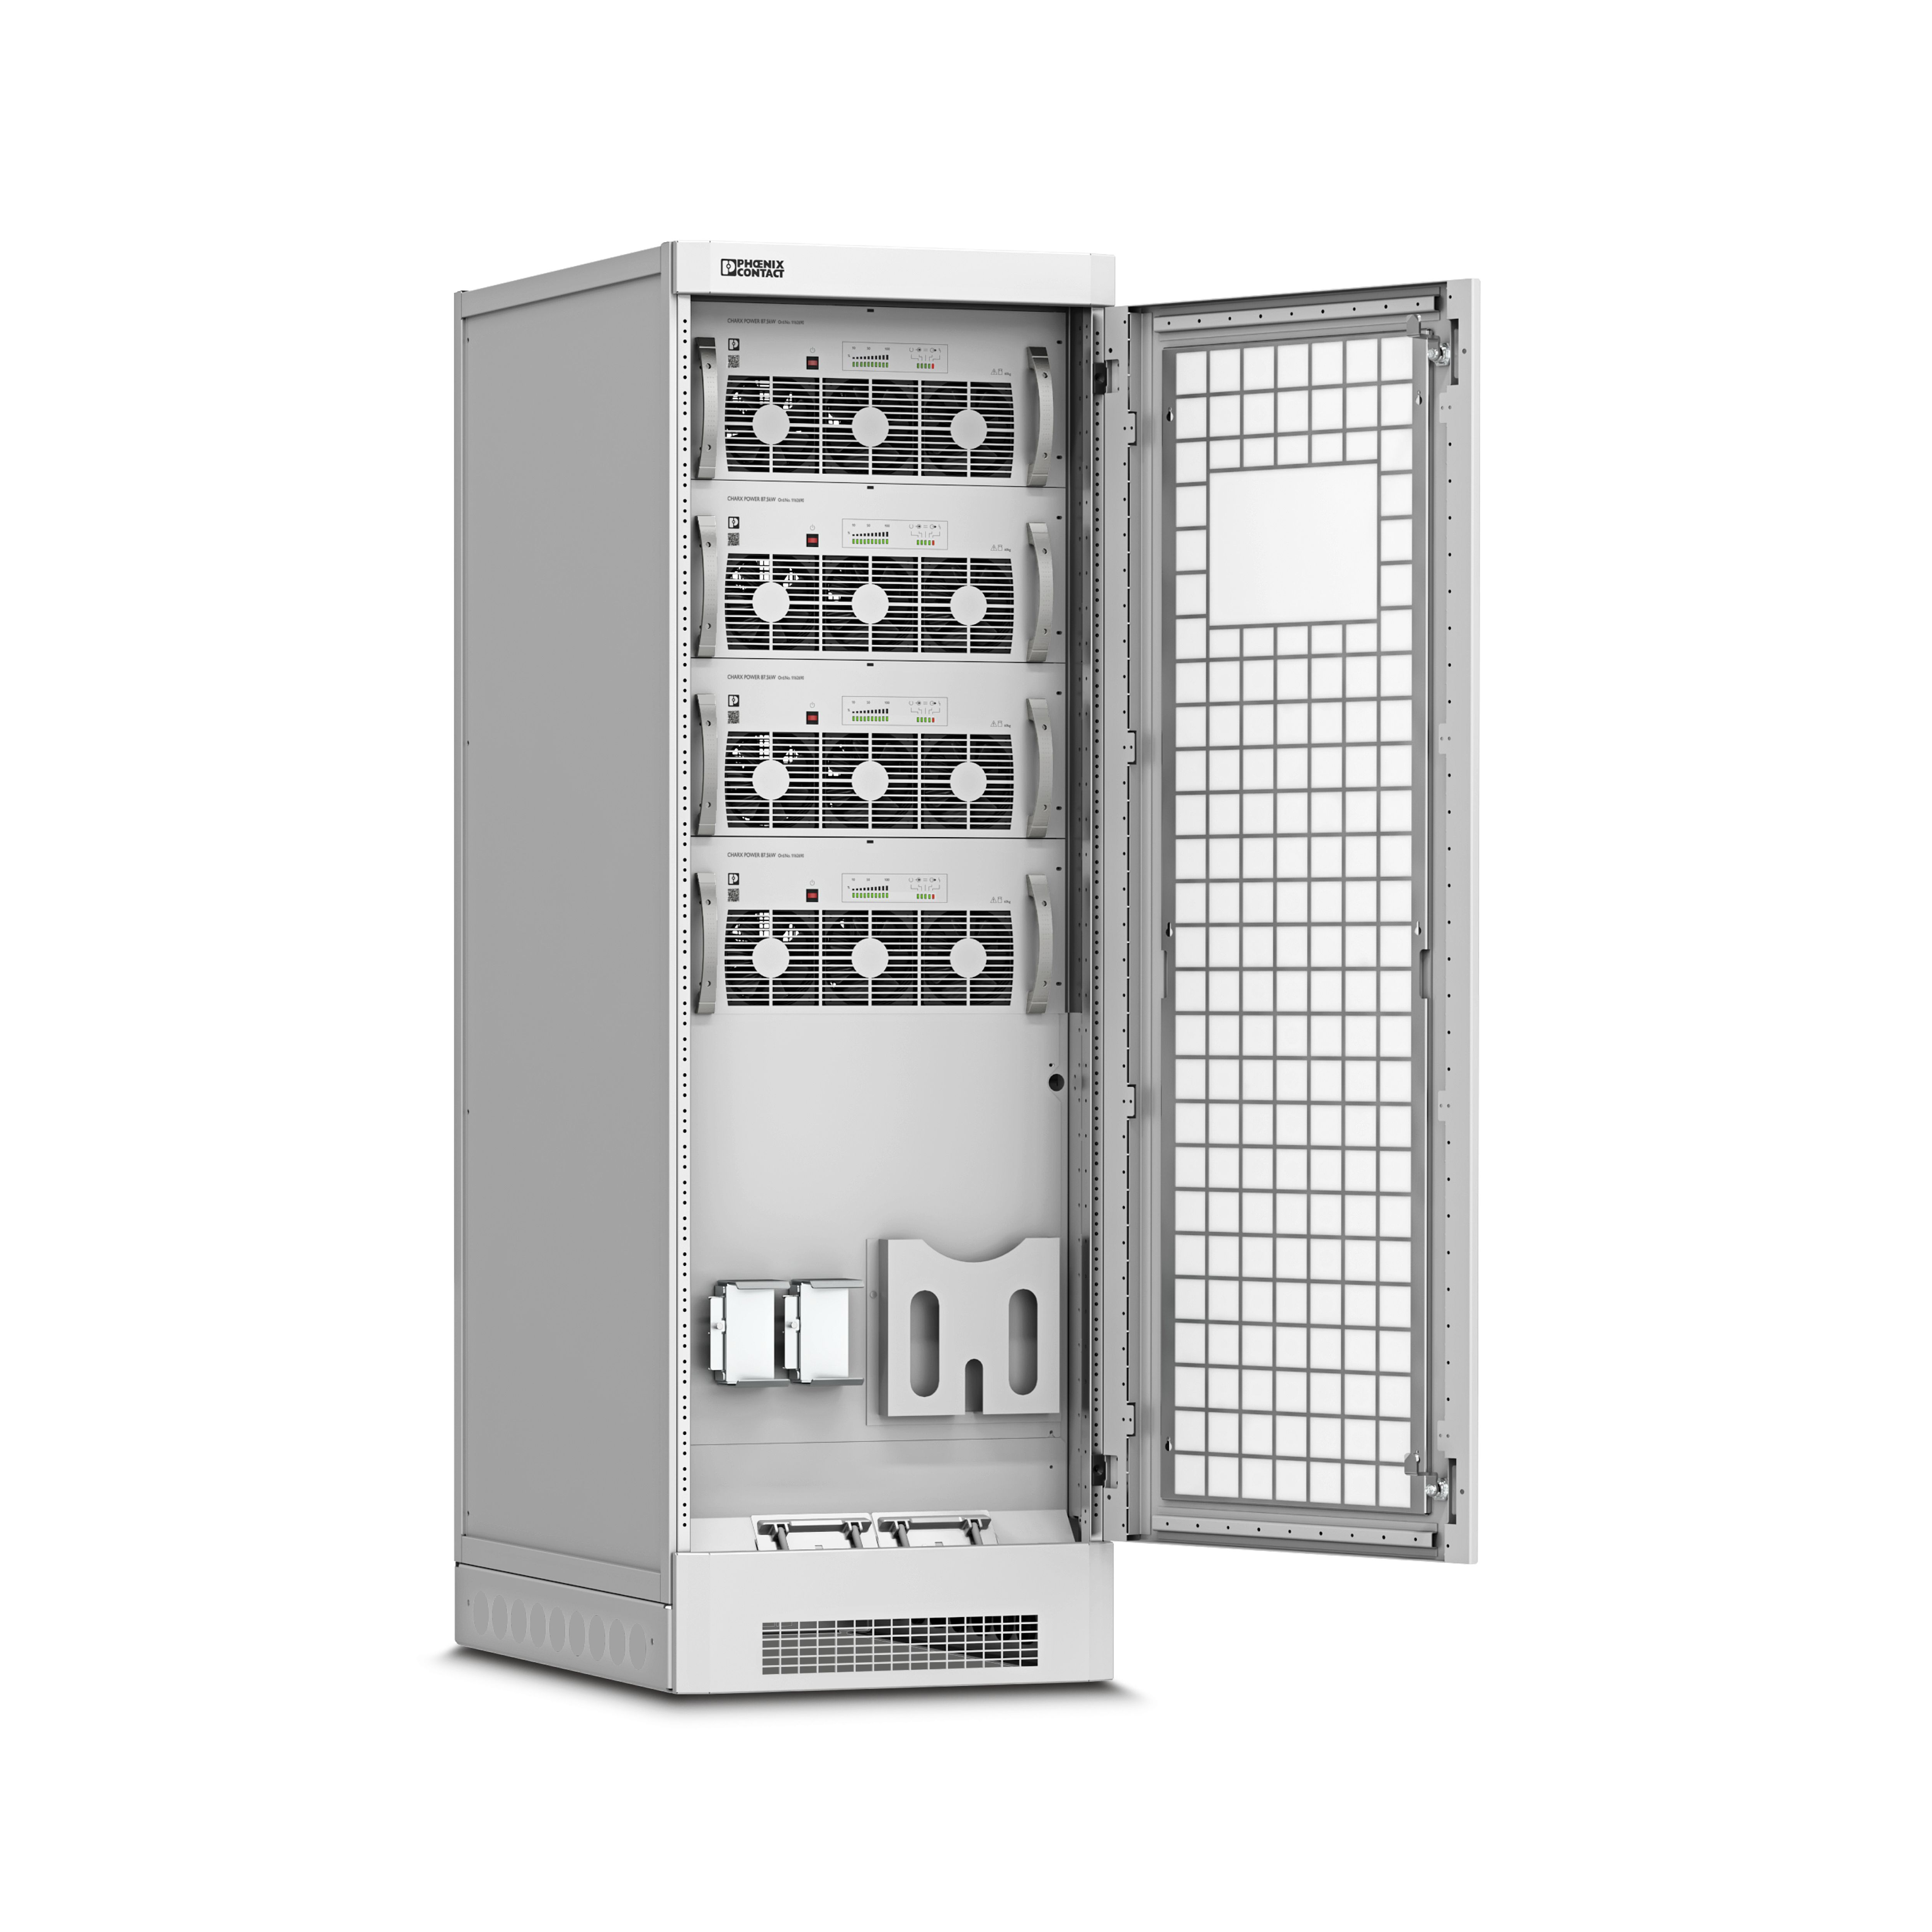
Most factories will remain connected to existing AC infrastructure. A bidirectional active infeed converter can exchange energy between the AC and DC grids, feed surplus energy back, and stabilize the network. DC/DC couplers segment the grid and integrate DC devices.
Protection demands particular care because DC has no regular zero crossing. Arcs can persist when circuits open or insulation fails. Suitable grounding concepts include a monitored DC IT system or a DC TN-S system grounded on the AC side.
Smart breakers enable arc-free, bidirectional disconnection. The ELR HDC-PT-24/650/55-IOL interrupts semiconductor current within 10 µs, then isolates both poles electromechanically. It also supports ground-fault, short-circuit, line, residual-current, overvoltage, and undervoltage protection. Arc analysis remains essential because tripping time directly affects arc energy and the personal risk assessment.
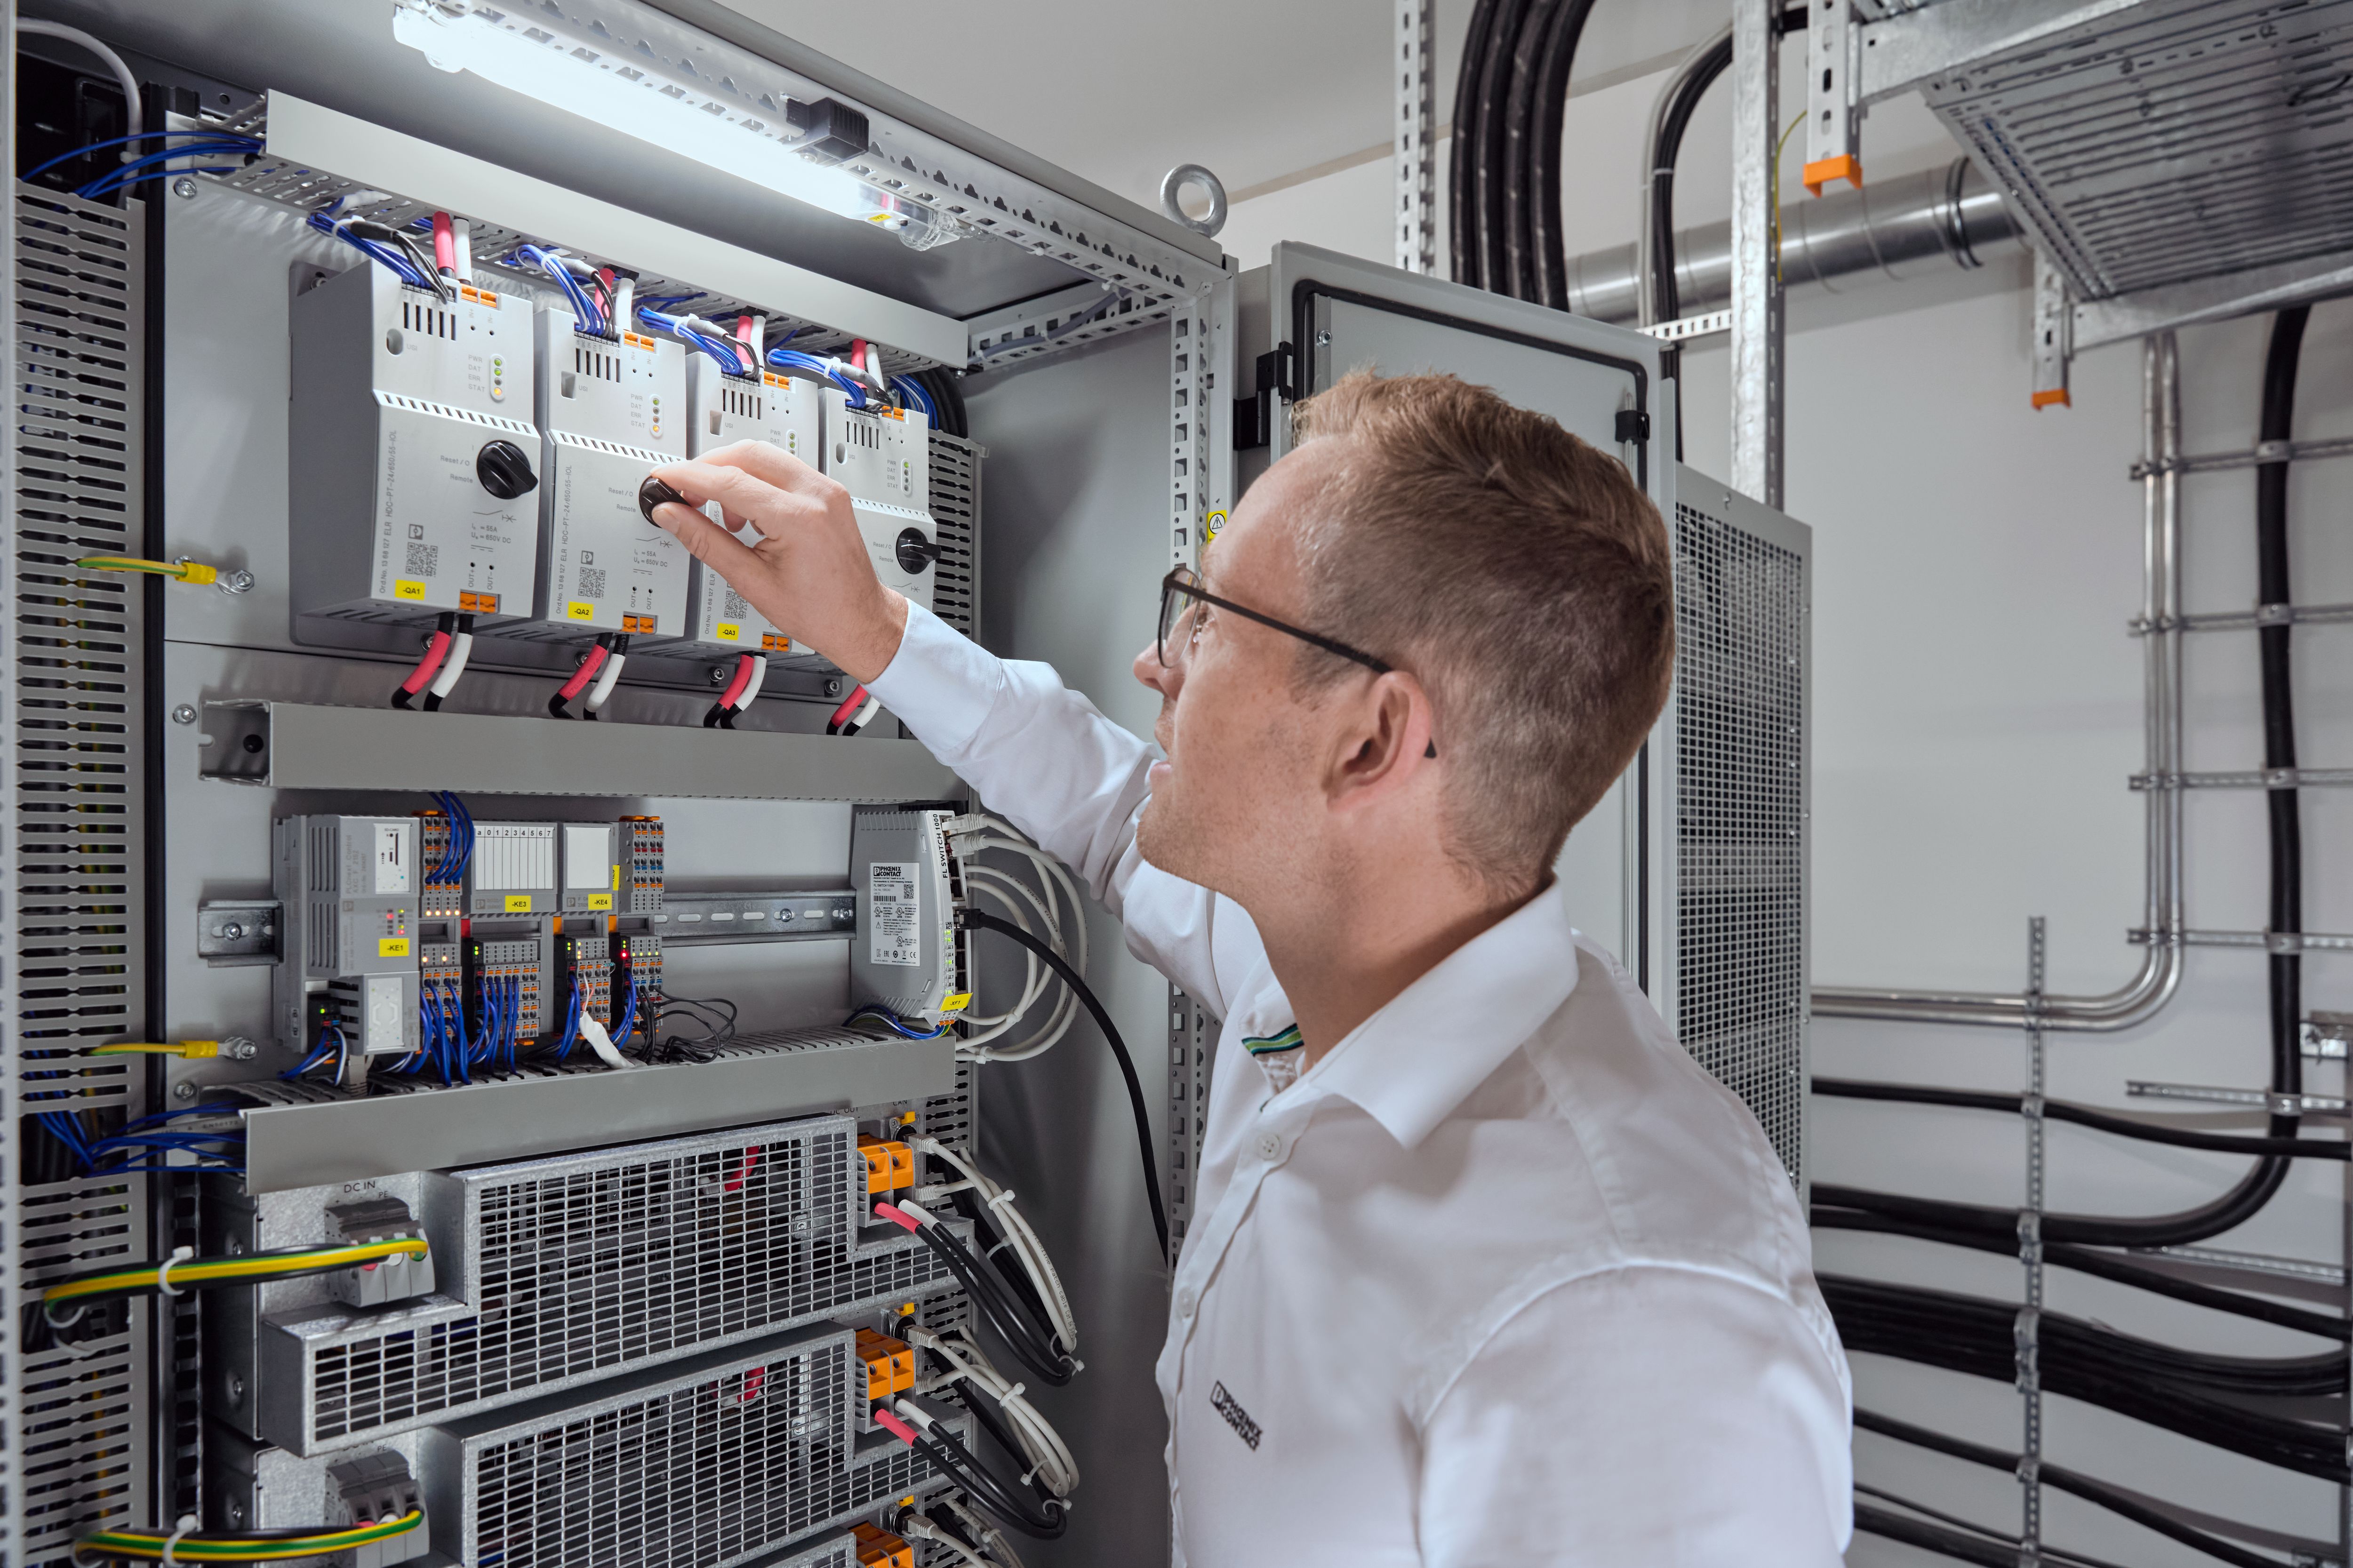
The ELR HDC-PT-24/650/55-IOL smart breaker being used at the Phoenix Contact DC factory
Manage energy without compromising availability
Production availability remains the priority. Primary droop control stabilizes bus voltage by coordinating sources, loads, and storage along U-I characteristic curves. Batteries or supercapacitors react quickly to peak loads, while the AC/DC converter regulates the base load near the lower voltage limit.
Secondary control can combine a PLCnext Control DC grid controller with Emalytics. This layer can limit peak loads, shift consumption, respond to electricity prices, prioritize PV self-consumption, manage battery state of charge, coordinate charging priorities, and optimize CO₂ performance.
From potential to practical implementation
A DC factory can increase the sustainable use of energy while reducing associated costs. The All Electric Society Factory demonstrates the approach through PV, battery storage, charging infrastructure, a partially integrated DC grid, heat pumps, and 1,500 m³ of ice storage. With more compatible products reaching the market, industrial DC grids are becoming not only sensible, but manageable.
Ready to explore the potential of a DC grid for your production environment?
Learn more about the technologies, components, and planning considerations for building a safe, reliable, and energy-efficient DC factory. Learn more about industrial DC grids
Modern switching devices must deliver more than operational safety and availability. They must also support resource conservation, occupational safety, and efficient operation throughout the system life cycle. As power electronics become more integrated into the grid, the frequency spectrum used to assess grid conditions expands, while conventional converters increasingly reach limits caused by nonlinear characteristics and saturation effects. Low-power instrument transformers, or LPITs, provide an alternative. Their compact design supports space-saving switchgear concepts for modern medium- and high-voltage systems. However, LPITs also change measurement and protection architectures. Instead of power-carrying secondary circuits, they provide low-level sensor signals. Consequently, periodic protection testing requires a new approach.
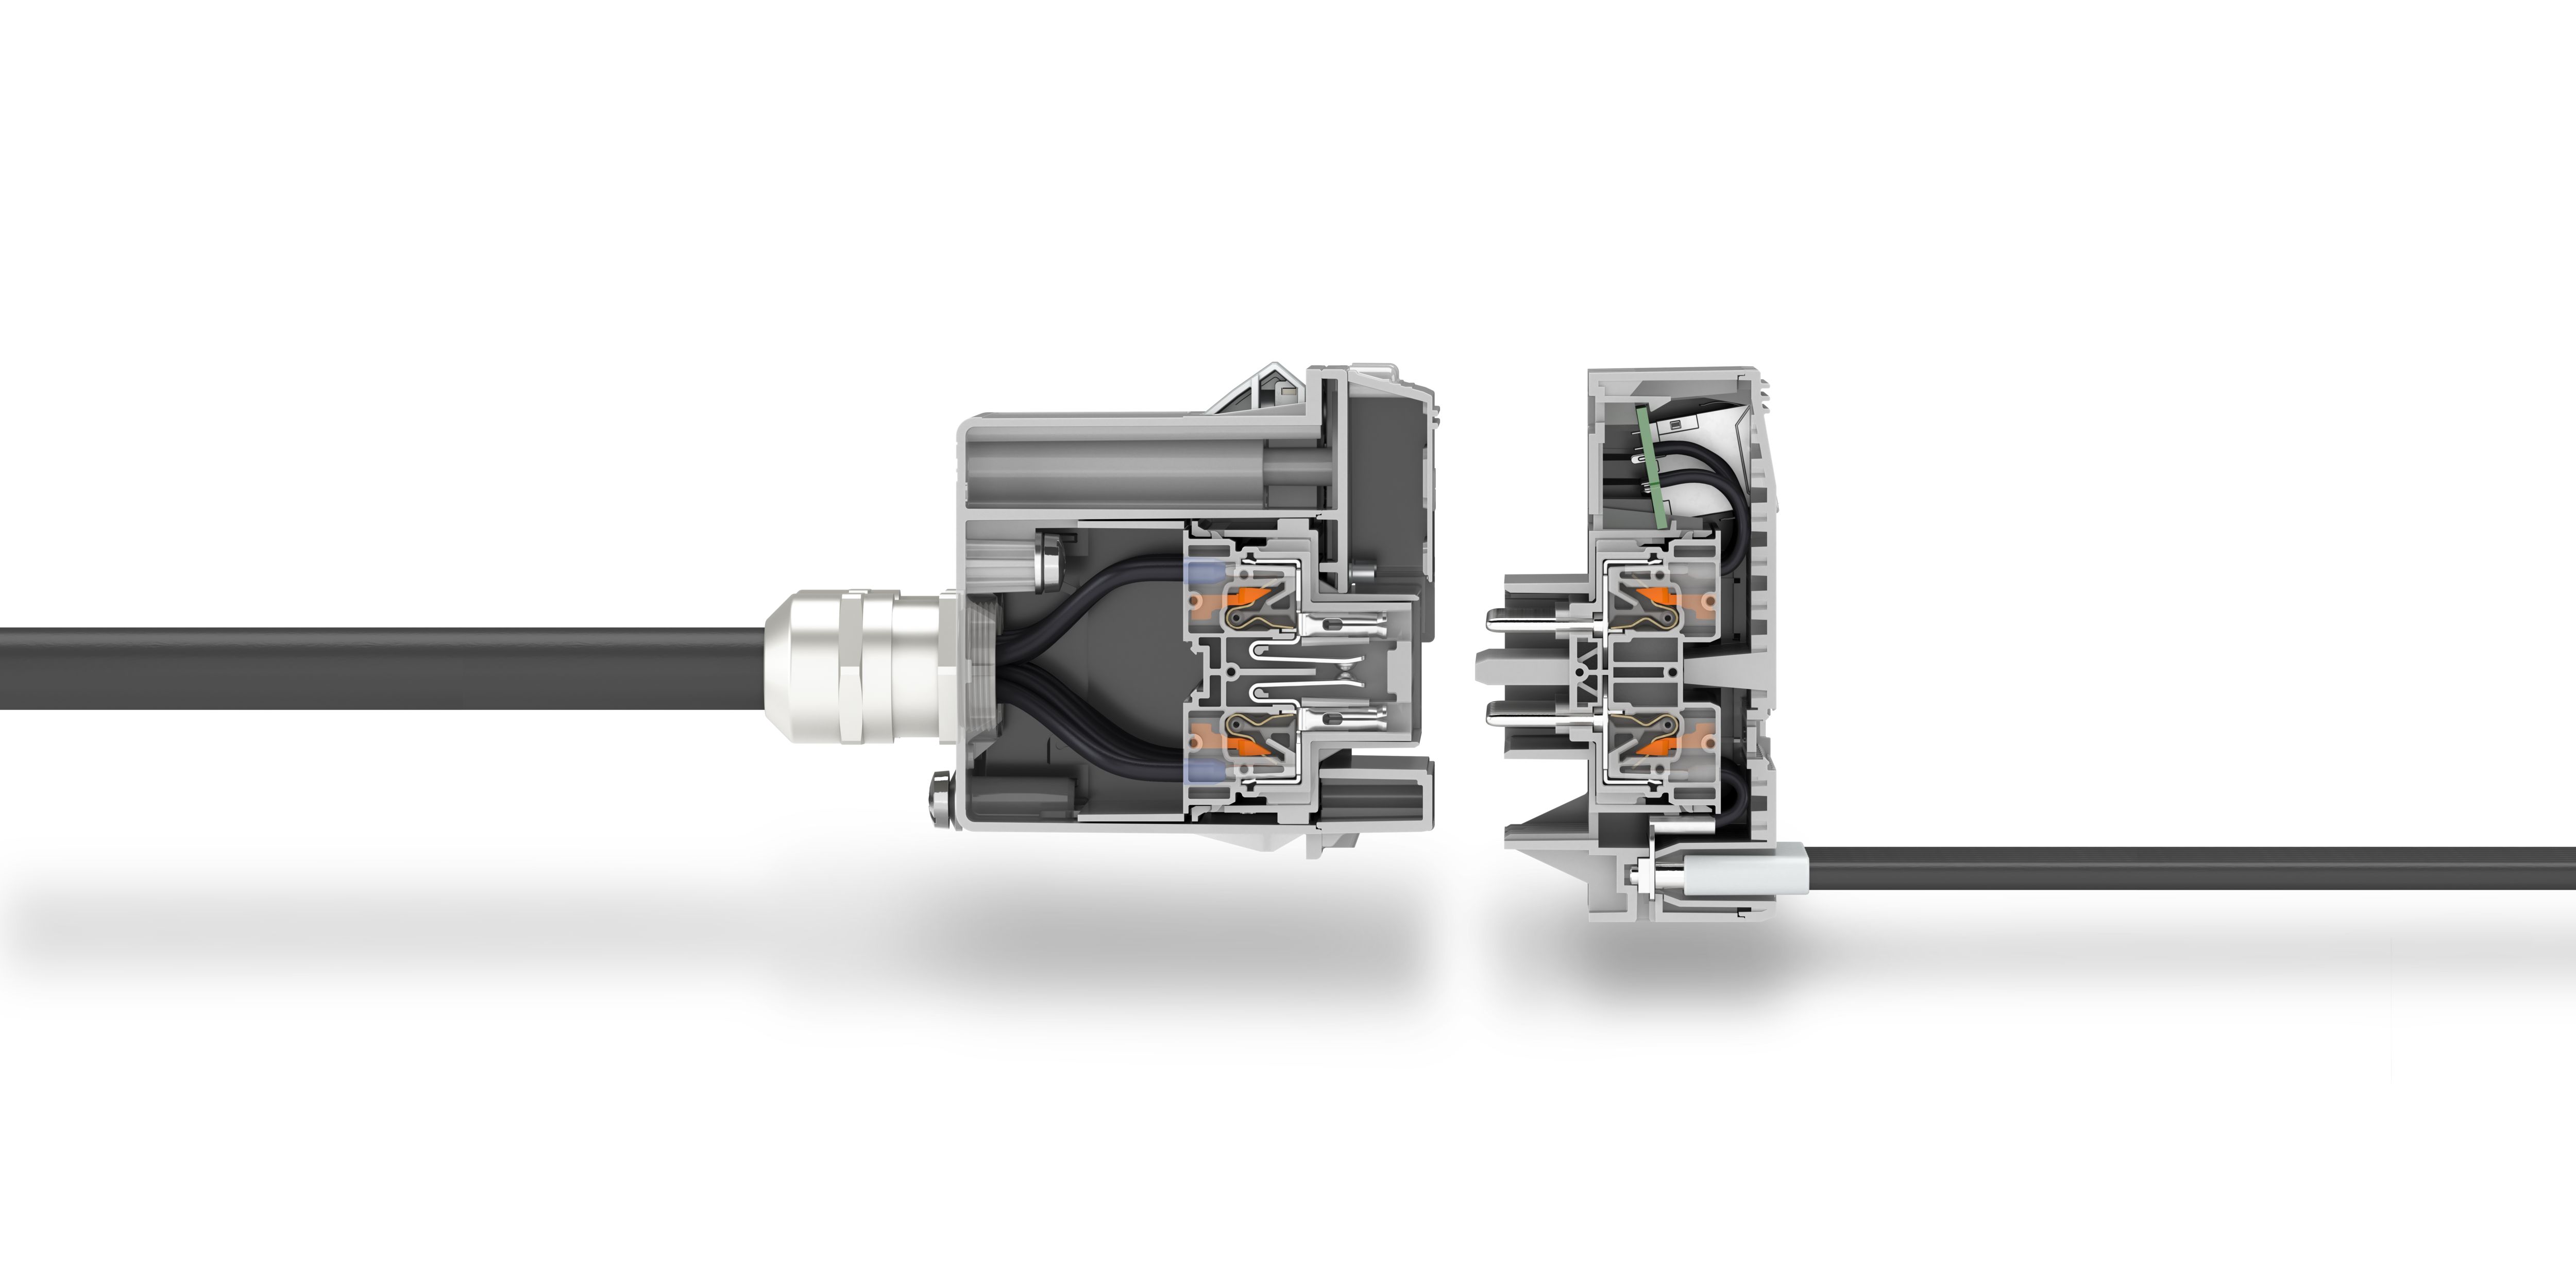
Cross-sectional view of Fame LPIT for standardized protection testing while the system is energized.
Why traditional testing methods fall short
Traditional testing methods are only partly suitable for LPIT-based switching devices. Manual wiring, serial switching, and changes to measurement circuits take time and introduce potential errors. They can also affect occupational safety, system availability, and operational processes. Operators therefore need a testing concept that provides reliable signal transmission and enables protection tests without disturbing existing wiring.
LPIT signals are more sensitive than conventional converter secondary circuits to electromagnetic interference, contact transitions, and inadequate shielding. For that reason, robust, continuous shielding is a fundamental system requirement.
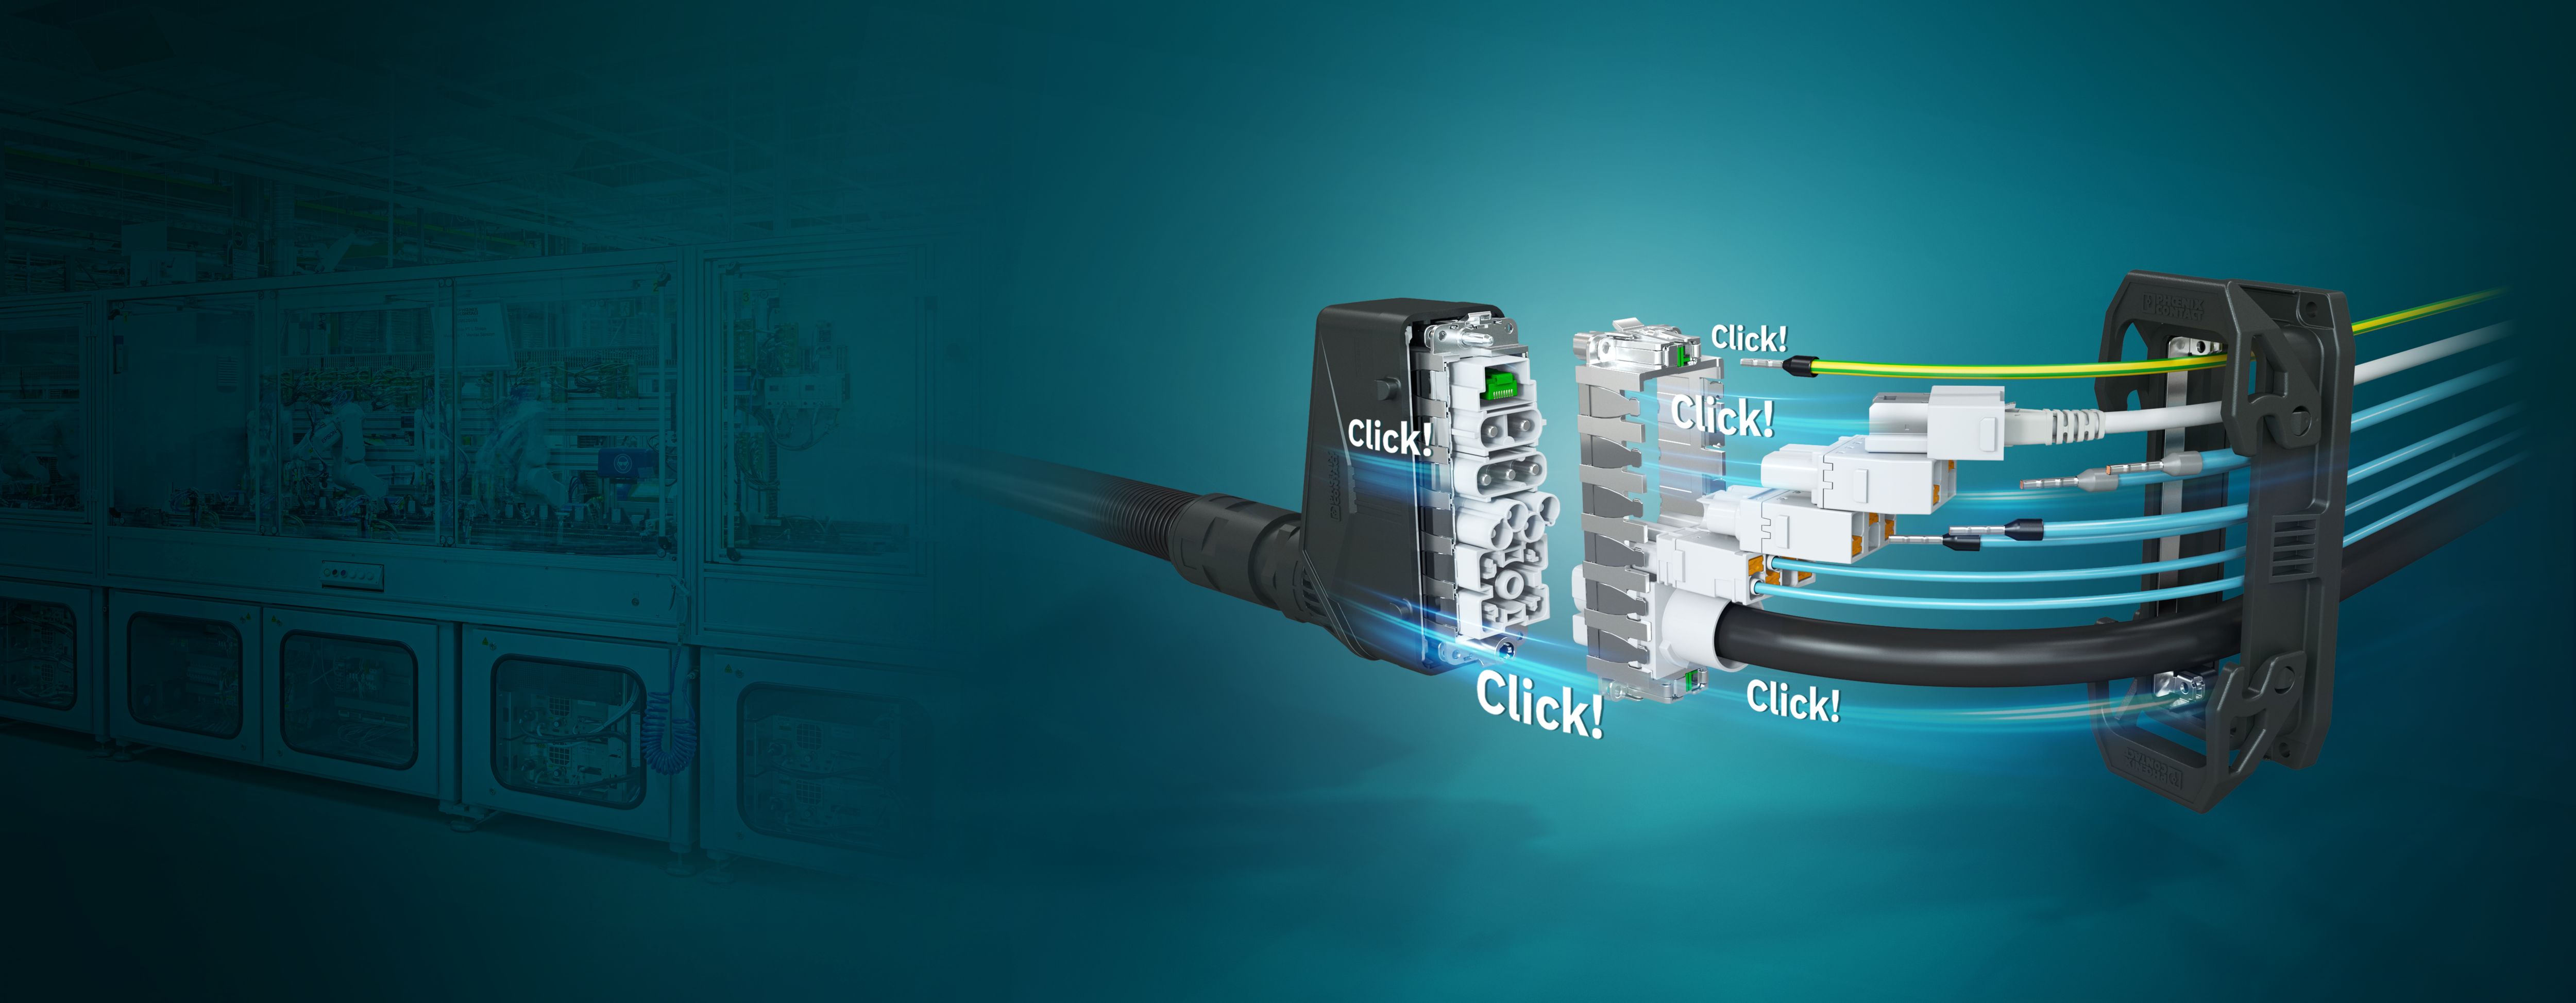
What challenges does the machine building and systems manufacturing industry face, and how can innovative connectors help address them? Simple, standardized connection processes that can be automated as much as possible are becoming a key driver of efficiency and system availability.
New contact inserts and module carrier frames for completely tool-free mounting
The machine building and systems manufacturing industry is facing profound challenges that are placing increasing pressure on established production processes. In many industrialized nations, experienced professionals are retiring from the workforce, while there is a shortage of qualified young talent. Technical professions that involve hands-on work and experience, such as mechanical engineering, systems manufacturing, and control cabinet building, are being hit especially hard.
Companies must therefore carry out complex electrical engineering tasks with fewer staff. The demands for flexibility, modularity, and cost-effectiveness are increasing, while times-to-market for new machines and systems are shrinking. Industrial companies expect customized solutions, short lead times, and rapid commissioning.
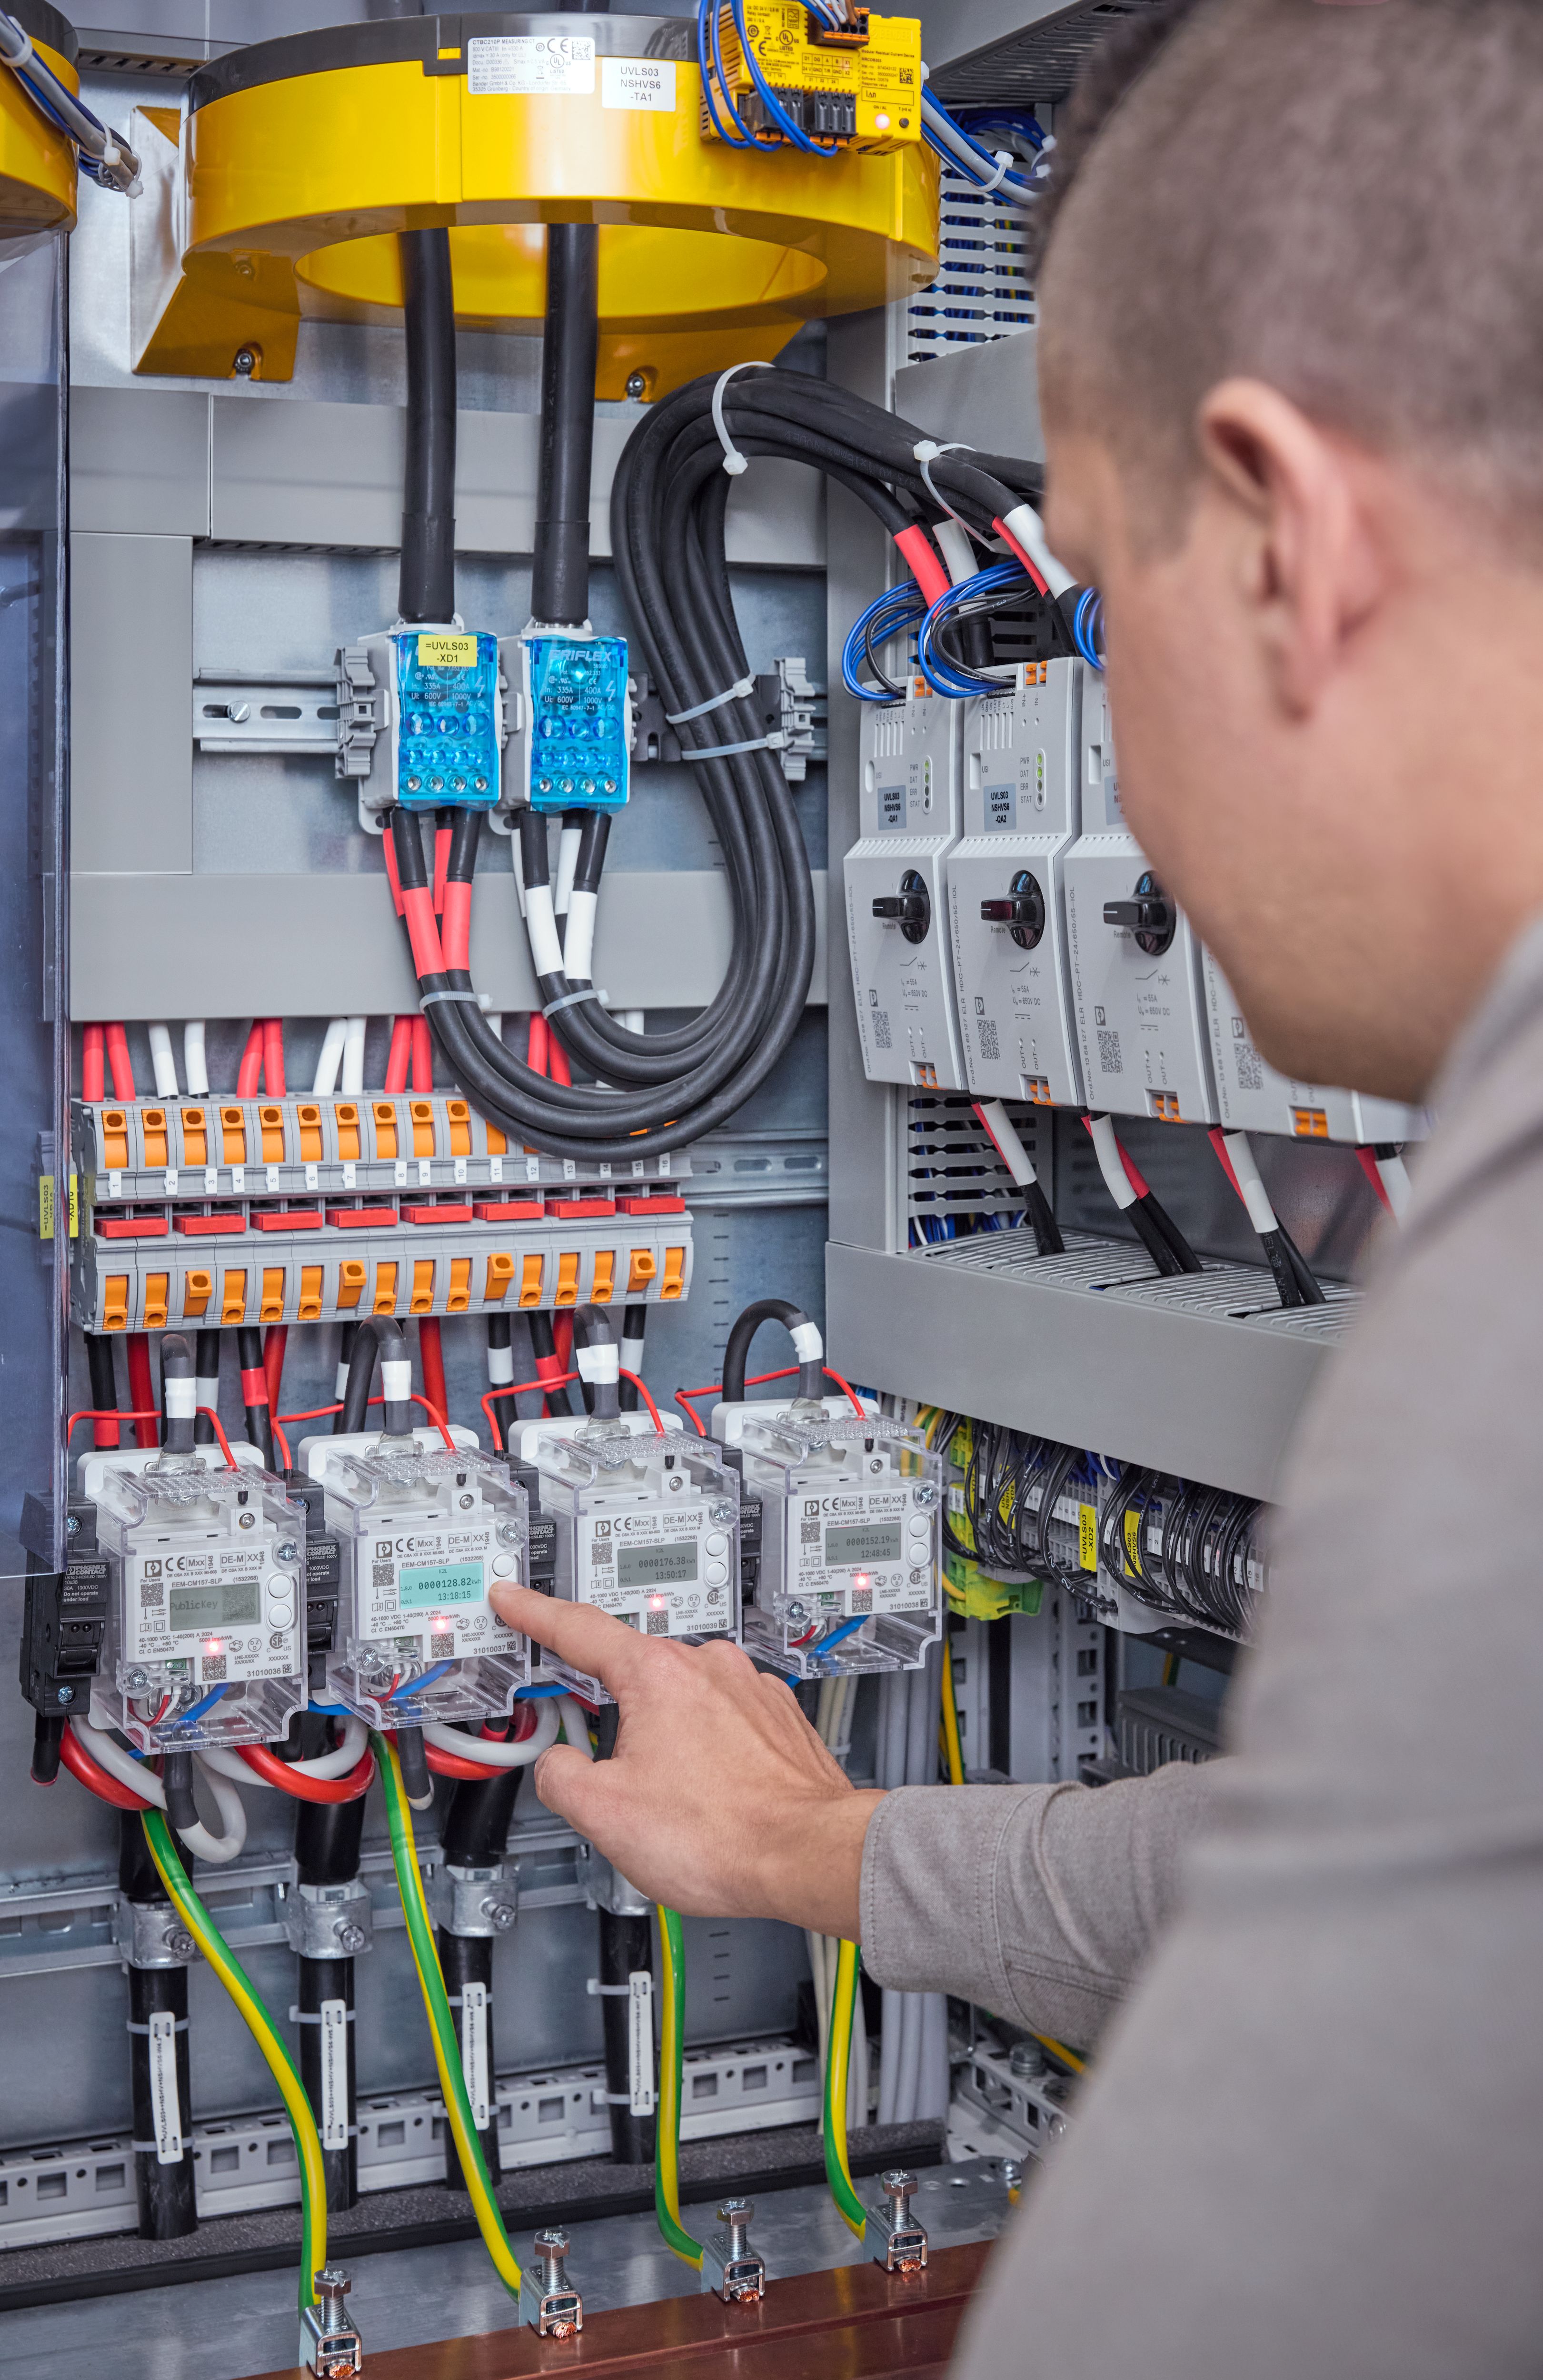
Lightning strikes and switching operations in the power grid can create surge voltages capable of disabling sensitive electronic systems. Routers, heat pumps, controllers, servers, photovoltaic inverters, and even complete production facilities may be affected. Although damaged hardware can be replaced, production downtime and data loss often create greater disruption and expense. The SPP surge protection system from Phoenix Contact provides a coordinated approach to protecting critical electrical and electronic infrastructure from lightning strikes and surge voltages. As modern buildings, industrial facilities, and photovoltaic systems become increasingly dependent on sensitive electronics, a single surge event can result in equipment damage, costly downtime, and data loss. The SPP family is designed to help ensure high system availability through end-to-end protection.
Two Coordinated Product Lines
The SPP family consists of two complementary product lines. FLT-SPP provides type 1+2+3 combined lightning current and surge protection, while VAL-SPP covers type 2 AC applications and type 1 or type 2 protection for photovoltaic systems. Their consistent design and safety concept simplify planning and help coordinate protection from the main distribution system through to sub-distribution.
The energy sector is undergoing a profound transformation. Increasing demands on sustainability, security of supply, and efficiency make smart solutions indispensable. Modern products and services for the energy management of the future combine technological innovations with a clear goal: using energy more intelligently, conserving resources, and improving cost-effectiveness. An energy management system must also be easy to implement. Coordinated sensor and measurement technology reduce the effort involved in energy data acquisition, while communication solutions and digital services help integrate, manage, and process measurement data. Companies are increasingly turning to intelligent hardware that provides transparency regarding energy flows and actively manages them.
Smart products, measurement technology, and digital services work together to provide transparency regarding energy flows and support intelligent energy management.
Measurement Technology as the Basis of Energy Management
In industrial and building structures, energy measurement technology forms the foundation for efficiency, cost transparency, sustainability, and electrical safety. In industry and production, measuring systems enable transparent monitoring of system operation, load management, predictive maintenance, and high system availability. Data centers use measurement technology to optimize power usage effectiveness (PUE) and improve failsafe performance through residual current monitoring.
Smart buildings rely on real-time data to network heating, ventilation, and lighting systems while supporting ISO 50001 energy management requirements. Measurement technology is also essential for charging infrastructure and renewable energy applications, where accurate measurements ensure both reliable billing and stable grid operation. Without measurement data, achieving decarbonization targets and identifying potential energy savings would not be possible.
Figure 1: Topological representation of an energy monitoring solution.
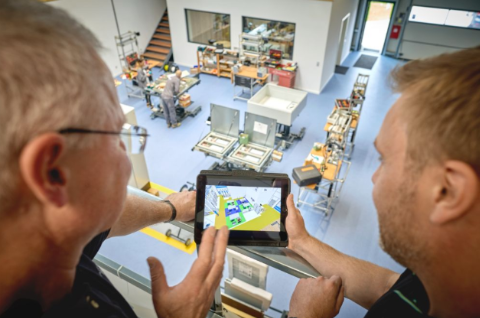
A 3D production layout forms the basis for structured, future-proof factory planning.
Control cabinet building efficiency has become a key priority for manufacturers. Rising demand, shorter delivery times, and increasing complexity put pressure on production teams. As a result, companies need production environments that are both flexible and efficient.
To address this challenge, Phoenix Contact and PGA partnered to modernize control cabinet manufacturing. Their project focused on two areas: factory planning and workstation design. Together, these improvements increased quality, reduced production times, and enhanced ergonomics.
The Growing Cybersecurity Challenge in Industrial Networks
As industrial systems become increasingly digital, they are unlocking new levels of efficiency and flexibility. But this transformation comes at a cost: greater exposure to cyberattacks. What was once limited to IT environments now directly affects operational technology (OT), putting production continuity and infrastructure reliability at risk in modern industrial network cybersecurity environments.
To address this growing threat landscape, cybersecurity is no longer optional—it’s becoming a regulatory requirement. Frameworks such as the IEC 62443 standards, along with European regulations like the NIS 2 Directive and the Cyber Resilience Act (CRA), are setting clear expectations for how industrial organizations must secure their systems. These regulations extend responsibility beyond critical infrastructure to include much of the industrial value chain, while also requiring security measures to be verifiable across a product’s lifecycle.
From Compliance to Industrial Network Cybersecurity in Practice
Meeting regulatory requirements is only the starting point. The bigger challenge lies in translating these standards into real, effective protection on the ground.
Industrial networks are made up of multiple interconnected components, each playing a role in maintaining security. Managed switches, security routers, and wireless infrastructure together form the backbone of modern industrial communication. But as connectivity increases—especially with remote access and wireless technologies—so does the number of potential entry points for attackers.
And the risks aren’t always obvious. Over time, misconfigurations, outdated firmware, or unsecured interfaces can quietly create vulnerabilities. In long lifecycle environments, these gaps can go unnoticed until they become critical.
Automated UV inkjet printing with the Bluemark E.Card
Industrial identification plays a key role in keeping modern systems running reliably. However, rising technical demands and structural constraints challenge control‑cabinet and machine builders. In response, Phoenix Contact’s new Bluemark E.Card UV inkjet printer shows how marking processes can be simplified and accelerated, improving overall efficiency.
In control cabinet and machine building, system functionality and availability are the priority. Consistent identification of installed components is essential but often overlooked. Clear, durable labeling improves orientation and streamlines workflows throughout a switchgear system’s lifecycle. Standards such as EN IEC 81346 define uniform reference designations for systems, devices, and functions, regardless of manufacturer.
Consistent identification of all components, devices, and circuits supports quality assurance, speeds commissioning, and enables quick responses during service or maintenance. As a result, industrial identification is crucial for the reliable operation and availability of modern systems.
Increasing demands on identification processes
Control cabinet and machine builders face growing challenges. With increasing system diversity and complexity, the technical demands on industrial identification are high. Applications range from protected control cabinets to machines where markings must withstand chemical and mechanical stress. This requires versatile solutions that deliver clear, high‑quality, and durable markings.
Control cabinet and machine builders also face structural challenges. A Germany‑wide study by Phoenix Contact and Ruhr University Bochum shows rising efficiency pressure across the industry. 88% of surveyed companies cite a shortage of skilled workers, and 62% report recurring capacity bottlenecks. Time‑consuming manual tasks, such as printing and processing marking materials, tie up qualified staff and worsen the situation. The industry’s project‑driven nature adds complexity, with 73% of sales coming from project business, leading to high product variety and demanding flexible production processes. Media discontinuities further slow workflows: despite digitalization, 88% of companies still receive planning data as PDFs and rely on paper documents, highlighting the need for more integrated processes industrial efficiency challenges.
To achieve consistent industrial identification, control cabinet and machine builders must do more than meet technical requirements. They need to simplify marking processes, reduce manual work, and better integrate digital workflows. Phoenix Contact addresses this with the new Bluemark E.Card UV inkjet printer, which sets new standards in efficiency and print quality for industrial identification.
Automated material processing meets innovative printing technology
High print volumes and diverse materials quickly overwhelm conventional card printers, especially when cards must be inserted and removed manually, an approach that is slow and error‑prone. The UV inkjet printer solves this with automated card transport: it feeds stacked materials into printing, then restacks them afterward, even detecting unsorted cards and marking them correctly. This automation saves time, up to 40% compared to manual processing, and boosts overall efficiency automated printing. Maintenance for cleaning or replacing fixed inkjet printheads is common and often causes downtime and reduced print quality. The Bluemark E.Card avoids this by using thermal inkjet technology, where the printhead is integrated into the ink cartridge. This ensures consistently high print quality and minimizes maintenance through regular cartridge replacement thermal inkjet technology.
Versatile identification solutions for industrial requirements
By combining thermal inkjet technology with UV‑LED‑curable inks, Phoenix Contact’s new card printer delivers high‑quality markings for all applications. The Bluemark E.Card automatically detects inserted materials and applies optimized print parameters for each one. Its modular ink system produces sharp text on polycarbonate, polyamide, and metal cards.
Thanks to intensive UV curing, the markings are wipe‑proof, scratch‑resistant, and chemical‑resistant, meeting the demands of durable identification in control cabinet and machine building industrial identification.
Consistent use of digital marking data
Efficient industrial identification requires consistent marking data and digitally integrated printing systems. Phoenix Contact’s marking software supports large projects and controls printers like the Bluemark E.Card, offering application‑focused functions and interfaces to ECAD tools and common data formats. With the Universal Data Interface, marking data can be used consistently without complex direct integrations. Information from digital circuit diagrams is easily imported for fast creation of marking solutions. Print projects are planned and monitored via the printer’s bidirectional OPC UA interface, while the Bluemark E.Card displays all key device and print status information.
Using digital data throughout the process reduces manual work, minimizes errors, and enables flexible marking, especially in project‑driven control cabinet building digital marking processes.